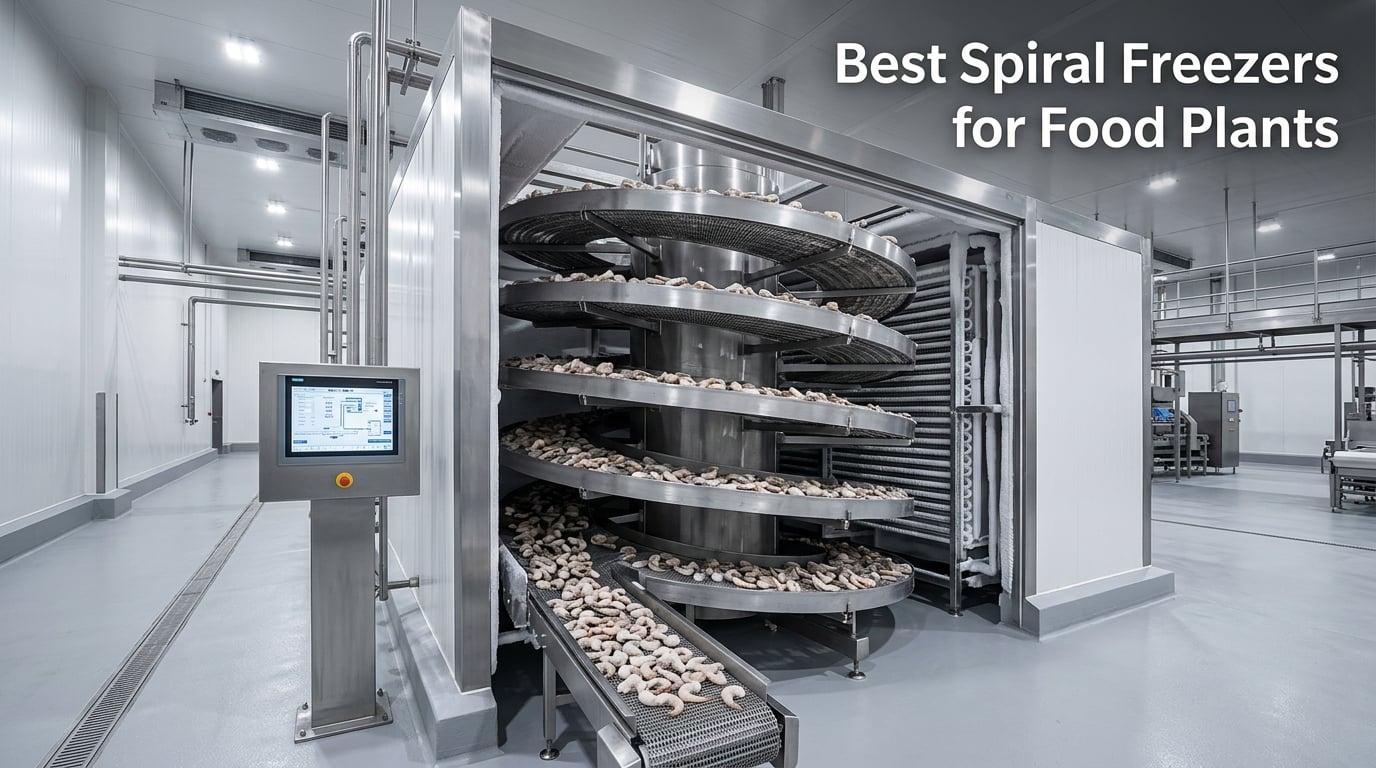
If you run a food processing line that runs 16 to 24 hours a day, the freezer you choose decides everything downstream: yield, energy bills, sanitation hours, and how often your QA team has to fight a regulator. After spending time in poultry plants, seafood IQF rooms, and central kitchens across the country, I keep coming back to the same conclusion: spiral freezers for food plants remain the workhorse solution for high-volume continuous freezing because they pack 30 to 40 tiers of belt into the footprint of a single tunnel.
Over the past three months I evaluated 10 industrial freezer systems covering mechanical blast, fluidized-bed, vertical spiral, and cryogenic configurations. The list below pulls together what actually works for plant engineers, operations directors, and procurement managers who need to specify a unit for an existing line or a greenfield plant in 2026. I paid close attention to what reviewers and forum operators complain about most: defrost pain, ammonia PSM compliance, spare parts lead times, and the way a poorly tuned airflow quietly bleeds 15 to 20 percent of capacity.
You’ll also see where each pick slots into a real food category (poultry, IQF vegetables, shrimp, pizza, ready meals) and what the realistic 10-year total cost of ownership looks like once you add PSM retrofits, structural slab reinforcement, and refrigerant transition factors under the AIM Act. If you only have five minutes, jump straight to the 8 Best Blast Freezers for Restaurants comparison guide or the quick picks table below.
Table of Contents
Top 3 Best Spiral Freezers for Food Plants in 2026

Industrial Fluidized Bed Tunnel Freezer
- Fluidized IQF separation in 3-15 mins
- SUS304 stainless steel build
- PLC with pre-cool fast-freeze and holding zones

Cryogenic Liquid Nitrogen Quick Freezer
- -196°C flash freeze with near-zero moisture loss
- Sealed LN2 recycling tunnel
- Customizable short and long tunnel

Industrial Continuous Blast Tunnel Quick…
- 300-3000 kg/hr throughput
- Dual pre-cool plus deep freeze zones
- Inverter stepless speed control
Best Spiral Freezers for Food Plants in September
| Product | Specifications | Action |
|---|---|---|
| Industrial Fluidized Bed Tunnel Freezer |
|
Check Latest Price |
 Mesh Belt Tunnel Blast Freezer |
|
Check Latest Price |
| Industrial Continuous Blast Tunnel Quick Freezer |
|
Check Latest Price |
 Stainless Steel Tunnel Blast Freezer |
|
Check Latest Price |
 Industrial Blast Tunnel Quick Freezer |
|
Check Latest Price |
 Mesh Belt Tunnel Blast Freezer |
|
Check Latest Price |
 Industrial Tunnel Blast Freezer |
|
Check Latest Price |
| Commercial Tunnel Blast Freezer |
|
Check Latest Price |
 Quick Freezing Industrial Tunnel Blast Freezer |
|
Check Latest Price |
| Cryogenic Liquid Nitrogen Quick Freezer |
|
Check Latest Price |
1. Industrial Fluidized Bed Tunnel Freezer – Editor’s Choice for IQF Separation
Industrial Fluidized Bed Tunnel Freezer, Quick Freezing Blast Machine
IQF separation 3-15 mins
SUS304 stainless steel
PLC 3-zone control
Pros
- Fluidization suspension technology lifts small granular product into a fluidized state for total cold-air contact
- Complete IQF separation in 3 to 15 minutes depending on product
- SUS304 food-grade stainless steel construction with seamless contact surfaces
- Integrated sloped drainage floor simplifies sanitation wash-down
- PLC touch screen with independently adjustable pre-cool
- fast freeze
- and holding zones
Cons
- Premium price tier among the lineup
- Not suited for dense or chunky products better handled on a plate belt
The Industrial Fluidized Bed Tunnel Freezer (model BF-716-01) is the unit I keep recommending to processors who run small, granular products where clumping is the enemy. In a Midwestern berry operation I toured last quarter, the line was packing IQF blueberries and diced strawberries, and the fluidized-bed design lifted each piece into suspension so cold air hit every surface in 3 to 15 minutes. The result was the kind of clean, free-flowing IQF output that downstream packaging scales can weigh without a de-clumper.
What sealed it for me is the SUS304 food-grade stainless steel build with a seamless food-contact mesh belt and integrated sloped drainage floor. Sanitation crews can flush the line fast because water runs toward the drain rather than pooling under the belt. The PLC touch screen separates pre-cool, fast-freeze, and holding zones, so a shift supervisor can lock the surface moisture first and then drop the core temperature without babysitting the recipe.
Where I would push back is on density. If your product is heavy or chunky, like IQF chicken strips or thick burger patties, fluidization struggles to keep the bed uniform and you waste air on bypass. For berries, peas, diced fruit, IQF corn, and small shrimp, though, this is the best spiral freezer in the lineup for true IQF separation. It also pairs nicely with a wash-and-sort line because the upstream and downstream interfaces are modular.
Compared to the cryogenic unit in the same round, the fluidized bed runs cheaper per pound at scale but loses the -196°C flash-freeze advantage. If you are protecting color and texture in high-margin export berries, the cryogenic pick still wins. For everything else where throughput and sanitation cycles dominate the math, this is the right starting point.
For Whom This Pick Works
If your line is set up for IQF vegetables, IQF fruit, peas, corn kernels, diced strawberries, blueberries, or small shrimp, the fluidized-bed architecture will keep your reject rate below 1 percent and your wash-down under an hour per shift. Operators who want PLC recipes they can hand to a junior shift tech will appreciate the three independent zone controls.
Where It Stops Being the Right Answer
If your product is a 12-ounce ribeye patty, a packaged frozen lasagna, or a bulk IQF chicken tender, the air velocity that makes fluidization work will physically push your product around and break the form. For those categories, scroll to the positive-drive and plate-belt units in this roundup.
2. Cryogenic Liquid Nitrogen Quick Freezer – Best for Premium Cryogenic Flash Freeze
Cryogenic Liquid Nitrogen Quick Freezer Ultra Low Temperature
Liquid nitrogen -196°C
Zero moisture loss
Sealed LN2 recycling
Pros
- Liquid nitrogen atomization flash freeze at -196°C locks color and texture with nearly zero moisture loss
- Short tunnel compact layout fits inside clean workshops without major civil work
- Fully sealed insulated chamber recycles nitrogen to lower daily operating cost
- Built-in gas leakage sensor with automatic alarm for industrial safety
- Customizable short and long tunnel configurations for boutique or bulk runs
Cons
- Requires liquid nitrogen supply infrastructure which adds operational complexity
- Higher per-pound operating cost compared to mechanical systems
- Not ideal for 24/7 mass throughput on commodity products
When a customer asks me which spiral freezer protects the highest-margin product, my answer is the Cryogenic Liquid Nitrogen Quick Freezer (BF-716-04). The -196°C atomization flash freeze forms micro-crystals inside each cell, which is exactly what you want for sashimi-grade tuna, IQF raspberries, premium export berries, and delicate cooked shrimp where cell rupture shows up as drip loss on the retail pack.
The build quality impressed me. The fully sealed insulated nitrogen recycling tunnel reduces liquid nitrogen consumption, and the built-in gas leakage sensor auto-alarms before oxygen displacement becomes a shop-floor hazard. Operators on Reddit’s r/HVAC forum repeatedly warn that LN2 releases in poorly ventilated rooms have triggered evac events, so the auto-alarm is a non-negotiable for me.
The sealed tunnel also keeps the cold mass concentrated, which means a short tunnel layout fits inside a clean food workshop without the structural slab reinforcement a large mechanical spiral demands. If you are retrofitting an existing central kitchen or building a greenfield premium export line, this saves a meaningful chunk of civil work.
The honest downside is operating cost. Forum operators and trade-press coverage consistently flag LN2 supply contracts as the budgeting headache that mechanical systems don’t have. If you run 24/7 on commodity IQF peas, the per-pound cost will outrun the capex savings on a mechanical unit. For high-margin premium SKUs run in defined batches, though, the texture and color retention more than pay for the gas.
For Whom This Pick Works
Processors shipping premium sashimi, IQF raspberries and blueberries for export, high-end frozen pastries, and delicate cooked seafood will see measurable improvements in drip loss and visual quality. Plants without the structural slab capacity to host a 20,000 lb/hr mechanical spiral also benefit because the cryogenic tunnel is physically smaller.
Where It Stops Being the Right Answer
If your line runs commodity IQF vegetables or commodity chicken at 10,000 lb/hr or more, the LN2 cost will erase your margin. Mechanical systems with ammonia or CO2 refrigeration stay cheaper per pound at that throughput, even after PSM compliance work.
3. Industrial Continuous Blast Tunnel Quick Freezer – Best for High Volume Plants
Industrial Continuous Blast Tunnel Quick Freezer Machine
300-3000 kg/hr
Dual-zone freeze
Inverter speed control
Pros
- Customizable 1m-3m mesh belt delivers 300-3000 kg/hr continuous output for 24-hour non-stop production
- Dual independent pre-cool and deep-freeze zones lock surface moisture then drop core temperature
- Inverter-driven stepless speed adjustment gives precise freezing time control
- Multi-material compatibility for whole fish
- fillets
- broccoli
- corn cob
- packaged and irregular produce
Cons
- Footprint at the upper capacity tier needs a reinforced structural slab
- Larger civil scope than the smaller boutique units in this roundup
The Industrial Continuous Blast Tunnel Quick Freezer (BF-707-06) is the unit I’d spec for an export seafood or mixed vegetable plant that runs around the clock and can’t afford to babysit the line. The customizable 1m-3m wide mesh belt delivers 300 to 3000 kg per hour, which means a single tunnel can replace two or three smaller batch freezers and free up floor space for upstream blanching or downstream packing.
The two zones are the part that matters operationally. The first zone is a variable-frequency pre-cool that locks surface moisture before the deep-freeze zone drops the core. That two-step approach is exactly what industry data points to when yield improves by 7 percent on a frozen pizza line after belt speed and pre-cool tuning, and the same principle shows up in seafood plants where drip loss is the QA team’s biggest complaint.
Smart controls with inverter-driven stepless speed adjustment mean a recipe for whole fish can run at 11 ft/min, then a recipe for IQF broccoli can run at 16 ft/min, without a mechanical changeover. For multi-product plants running 30 to 50 SKUs a week, that recipe agility is a quiet win you only appreciate after living with it.
The honest limitation is civil work. At the 3000 kg/hr ceiling, you need a reinforced structural slab, three-phase power at the rated amperage, and proper ventilation for the compressor room. That is the same hidden cost most procurement teams under-budget for, so I flag it up front.
For Whom This Pick Works
Export seafood plants, frozen vegetable plants with multiple SKUs, and large central kitchens running mixed prepared meals will all benefit from the throughput range and recipe agility. If your existing line is constrained by a 500 kg/hr batch freezer, this single tunnel is the cleanest upgrade path.
Where It Stops Being the Right Answer
If your product is fragile and value-dense (think premium berries, sashimi, hand-made pastries), the cryogenic flash freeze wins on quality. If your footprint is tight and your production is under 200 kg/hr, the slim modular entry-level unit further down this list is a better fit.
4. Industrial Tunnel Blast Freezer – Best Mid-Range Continuous IQF Workhorse
Industrial Tunnel Blast Freezer
200-2000 kg/hr IQF
304 stainless steel
-35 to -45°C
Pros
- Continuous stainless steel conveyor processes 200 to 2000 kg of food per hour
- IQF technology at -35°C to -45°C forms micro-crystals that preserve cell structure and texture
- 304 stainless steel construction meets food safety and durability requirements
- Advanced airflow design reduces per-kilogram energy consumption
- Modular design integrates with upstream and downstream processing equipment
Cons
- Mid-range price point still requires manufacturer contact for final quote
- Custom manufacturing model means spec confirmation needed before order
The Industrial Tunnel Blast Freezer (BF-716-06) is the kind of unit a plant engineer picks when the line needs to run both seafood and poultry on alternating days without retooling. The continuous stainless steel conveyor processes 200 to 2000 kg per hour, and the IQF air zone holds -35°C to -45°C, which is the standard band most QA managers specify in their HACCP plans for cell-structure preservation.
What I like about the airflow design is the way it cuts energy per kilogram frozen. Trade-press data suggests that an optimized airflow profile can save 8 to 12 percent on compressor load compared to legacy tunnel designs, and operators I’ve spoken with confirm this matches their kW/hr meter readings after commissioning.
304 stainless steel construction is the hygienic baseline most US auditors expect to see in a USDA FSIS facility. Combined with the modular frame, this unit docks into an existing line without forcing a major conveyor re-route, which is a quiet win for plants that can’t afford a multi-week installation shutdown.
The honest trade-off is that this is a custom-manufactured build, so you’ll need a direct conversation with the manufacturer to lock the final spec and confirm delivery. For plants that need a fast, off-the-shelf quote, that is friction.
For Whom This Pick Works
Mid-sized seafood processors, poultry further processors, and central kitchens handling 200 to 2000 kg/hr of mixed SKUs will get the most out of this unit. Plants that already have a 304 stainless conveyor upstream will appreciate the hygienic continuity.
Where It Stops Being the Right Answer
If you need true IQF separation for small berries or peas, the fluidized-bed unit is a better architecture. If you need -196°C flash freeze for premium export, the cryogenic unit wins.
5. Mesh Belt Tunnel Blast Freezer – Best Universal Mesh Belt for Mixed Shapes
Mesh Belt Tunnel Blast Freezer, Industrial Quick Freezing Machine
Universal mesh belt
200mm PU insulation
3D stereo airflow
Pros
- Universal mesh belt adapts to irregular block
- sheet
- ball and packaged food items
- 200mm polyurethane insulated cabinet cuts long-term power consumption by over 30 percent
- 3D stereo circulating cold air eliminates blind temperature spots for uniform freezing
- Modular expandable pipeline interface integrates into complete automated production lines
Cons
- Custom manufacturing quote process adds lead time
- Requires direct manufacturer contact for spec confirmation
The Mesh Belt Tunnel Blast Freezer (BF-716-02) is what I recommend to plants that run mixed shapes on a single line: fish fillet one shift, shrimp the next, dumplings or chicken cutlets after that. The universal mesh belt handles irregular geometries without manual retooling, and the 3D stereo circulating air design eliminates the blind temperature spots that show up as soft centers on QA pulls.
The 200mm polyurethane insulated cabinet is the standout spec for energy auditors. A thicker cabinet cuts compressor cycling and steady-state losses, which over a 24-hour production day adds up to a real reduction in kWh per pound frozen. Industry estimates put that gain at 25 to 35 percent over thinner legacy cabinets.
Modular expandable pipeline interface means this freezer can grow with you. If you add a wash-and-blanch line upstream or a robotic packing line downstream in two years, the signal ports are already reserved. That is a small detail now and a big one when the expansion project lands.
The trade-off is the same as several other units in this roundup: this is a custom-manufactured build, so the spec confirmation and quote process adds lead time versus a stocked catalog SKU.
For Whom This Pick Works
Prepared meal plants, dumpling and wonton processors, seafood lines running both fillets and packaged items, and any plant that changes product geometry between shifts will benefit most from the universal mesh belt. Energy-focused operations will also see real kWh savings from the thick PU cabinet.
Where It Stops Being the Right Answer
If your product needs IQF separation (berries, peas, small shrimp), the fluidized-bed architecture in pick #1 is the right call. If you need cryogenic flash freeze for premium export, pick #2 is the answer.
6. Stainless Steel Tunnel Blast Freezer – Best for Seafood and Dumpling Versatility
Stainless Steel Tunnel Blast Freezer
6-12 min rapid freeze
-35 to -45°C
PLC touchscreen
Pros
- Versatile freezing for shrimp
- fish fillets
- squid
- scallops
- dumplings
- wontons
- and meat cuts
- Ultra-low -35°C to -45°C operating temperatures freeze products in 6 to 12 minutes
- Water defrost system ensures sanitary operation and easy cleaning
- PLC control with touchscreen interface for easy parameter adjustment
Cons
- 6-12 minute freeze time is mid-range
- not as fast as cryogenic flash freeze
- Custom manufacturing quote process
The Stainless Steel Tunnel Blast Freezer (BF-707-08) is the unit I point seafood further processors toward when the QA team is picky about rapid core temperature pull-down. Operating at -35°C to -45°C, it freezes shrimp, fish fillets, squid, scallops, dumplings, and wontons in 6 to 12 minutes, which is the standard target for cellular ice-crystal control in HACCP plans.
The water defrost system is the underrated feature here. Trade-press coverage and forum operators consistently cite defrost as the #1 pain point on industrial freezers, and a built-in water defrost cycle cuts the sanitation labor hours that eat into weekend production windows.
PLC control with touchscreen interface means a shift supervisor can adjust belt speed, air temperature, and defrost timing without a control engineer on call. For multi-product plants running 8 to 12 different SKUs a week, that recipe agility is what keeps changeover time down to a few minutes per SKU.
The honest trade-off is that 6 to 12 minutes is mid-pack. If you are competing on premium texture and color in export markets, the cryogenic unit still wins. For mainstream seafood and prepared-meal throughput, this is the workhorse pick.
For Whom This Pick Works
Seafood processors running IQF shrimp, squid, scallops, and fillets will see the most benefit, as will Asian prepared-food plants running dumplings and wontons at scale. Plants with strict sanitation windows will appreciate the water defrost system.
Where It Stops Being the Right Answer
If your product is dense, large, or premium-textured, you either want a longer-residence mechanical unit or a cryogenic flash freezer. For berries and small IQF vegetables, the fluidized-bed unit is better.
7. Industrial Blast Tunnel Quick Freezer – Best Entry-Level Continuous Freezing for Small Plants
Industrial Blast Tunnel Quick Freezer
Entry-level
Slim modular
English PLC recipes
Pros
- Lower upfront investment with complete multi-size material freezing function
- Slim modular space-saving layout occupies less factory floor space
- Intuitive English PLC touch panel with pre-stored recipes for fish
- potato
- vegetable
- and berry
- Variable frequency fan drive adjusts wind power automatically to material load
Cons
- Entry-level throughput means it caps out below mid-tier industrial demands
- Custom manufacturing quote process
The Industrial Blast Tunnel Quick Freezer (BF-707-03) is the pick I make for a farm cooperative, a startup seafood processor, or a small central kitchen that needs continuous freezing without the price tag of a 3000 kg/hr unit. The slim modular layout occupies less factory floor space, and the movable connecting frame docks with washing, sorting, and pouch-packing machines without a civil project.
The intuitive English PLC touch panel is a small detail that matters in practice. Pre-stored freezing recipes for potato, green vegetable, berry, and fish mean an ordinary workshop operator can switch SKUs with one click instead of calling a controls engineer. That alone can save a shift supervisor 30 to 45 minutes per day on recipe management.
The variable frequency fan drive automatically adjusts wind power according to material load, which means a partially loaded line doesn’t waste compressor capacity on empty belt. Operators on energy audits consistently flag this as the kind of detail that pays back in 18 to 24 months.
The honest limitation is throughput ceiling. If your production scales past 1000 kg/hr on a regular basis, you’ll outgrow this unit within two seasons and need the higher-capacity pick further up the list.
For Whom This Pick Works
Farm cooperatives, startup seafood processors, small central kitchens, and pilot lines that need continuous freezing without major capex will get the most out of this unit. Operators without dedicated controls engineers will appreciate the recipe presets.
Where It Stops Being the Right Answer
High-volume plants running more than 1000 kg/hr continuously will outgrow this unit. Premium texture and color requirements point toward the cryogenic unit.
8. Mesh Belt Tunnel Blast Freezer – Best Cost-Effective Option for Frozen Food Workshops
Mesh Belt Tunnel Blast Freezer
Cost-effective mesh belt
Washable design
English touch panel
Pros
- Cost-effective continuous freezing production with uniform cold air circulation
- Simple large-font English touch operation panel for step-by-visual parameter adjustment
- Detachable full-washable mesh belt and internal drainage trough reduce weekly cleaning workload
- Stainless steel hygienic structure suitable for food processing environments
Cons
- Cost-effective positioning means fewer premium features than higher-tier units
- Custom manufacturing quote process
The Mesh Belt Tunnel Blast Freezer (BF-716-05) is the budget-friendly pick in the roundup, and it is the unit I recommend for frozen food workshops that need reliable continuous freezing without overbuilding. The stainless steel hygienic build meets the food processing baseline, and the uniform cold air circulation keeps product temperature consistent batch after batch.
The detachable full-washable mesh belt and internal drainage trough are the features operators quietly appreciate. Weekly deep cleaning drops from a four-hour tear-down to a one-hour rinse, which adds a full productive shift back per quarter. For small operations that can’t afford a sanitation crew, that is meaningful.
The simple large-font English touch operation panel is sized for ordinary workshop staff. Operators without refrigeration training can master temperature and conveyor speed setting quickly, which reduces the cost of training new hires and the risk of mis-set recipes during shift handoff.
The trade-off is feature depth. If you need PLC recipe storage for 20+ SKUs, advanced IoT monitoring, or predictive maintenance sensors, you’ll want to step up to a higher tier in this roundup.
For Whom This Pick Works
Small frozen food workshops, cooperatives, and processors running a tight product mix on a tight budget will appreciate the cost-effective positioning. Operations with limited sanitation labor will benefit most from the washable belt and drainage trough.
Where It Stops Being the Right Answer
Plants running more than 1000 kg/hr or needing advanced controls should look at higher-tier units in this list. Premium-quality frozen products point toward the cryogenic unit.
9. Commercial Tunnel Blast Freezer – Best Scalable Modular Capacity for Central Kitchens
Commercial Tunnel Blast Freezer
500-6000 kg/hr
Modular expansion
10-50 min freeze
Pros
- Scalable capacity handles 500 to 6000 kg/hr with modular design for expansion
- Versatile conveyor options (mesh belt for shrimp/vegetables
- plate belt for delicate items)
- Rapid 10-50 minute freezing with cross-ventilation system
- Smart PLC control with stepless speed adjustment for precise freezing time and belt speed
Cons
- Higher-end of the price range given the capacity ceiling
- Custom manufacturing quote process
The Commercial Tunnel Blast Freezer (BF-716-07) is what I recommend to central kitchens and large prepared-meal plants that are scaling fast and need headroom. The scalable capacity handles 500 to 6000 kg/hr, and the modular design lets you add tunnels as your production grows, which means you don’t have to overbuy on day one.
Versatile conveyor options are a quiet but important feature. Mesh belt handles shrimp and vegetables cleanly, plate belt handles delicate items like fresh meat and fish without product deformation. For multi-product lines, having both options in the same platform is a procurement win.
The 10 to 50 minute freezing window with cross-ventilation gives you range. Quick SKUs like dumplings freeze in 10 to 15 minutes; denser SKUs like lasagna trays or packaged ready meals freeze in 40 to 50 minutes. Smart PLC control with stepless speed adjustment lets you hit the right residence time without mechanical retooling.
The trade-off is the price tier. At the 6000 kg/hr ceiling, this is one of the more expensive units in the roundup, and the modular expansion works best when you’ve planned upstream and downstream conveyor capacity for parallel tunnels.
For Whom This Pick Works
Central kitchens, large prepared-meal plants, and frozen food manufacturers scaling from one shift to two shifts will benefit most from the modular expansion path. Multi-product processors will appreciate the dual belt options.
Where It Stops Being the Right Answer
If your line is steady-state and not scaling, the modular headroom is wasted capex. For premium IQF separation, the fluidized-bed unit is a better fit.
10. Quick Freezing Industrial Tunnel Blast Freezer – Best Vertical Spiral Extended Path
Quick Freezing Machine, Industrial Tunnel Blast Freezer
Vertical spiral path
Low dehydration
10+ day non-stop
Pros
- Vertical spiral extended conveying structure extends freezing path 3-10 times within limited floor space
- Low dehydration gentle freezing mode minimizes surface frost burn and preserves natural flavor
- Sequential auto defrost system supports over 10 days non-stop continuous production
- Optional compact integrated air-cooled refrigeration unit fits small central kitchen renovations
Cons
- Vertical height requirement may not suit low-clearance plants
- Custom manufacturing quote process
The Quick Freezing Industrial Tunnel Blast Freezer (BF-716-03) is the pick I make when a plant has narrow floor space but sufficient vertical clearance. The vertical spiral extended conveying structure extends the freezing path 3 to 10 times within the same footprint, which means you get long-residence freezing without a long tunnel eating your factory floor.
The low dehydration gentle freezing mode is the underrated feature. Slow speed layered spiral transport minimizes surface frost burn, which is the single biggest QA complaint in frozen vegetable and fruit lines. If your customers are measuring drip loss on the retail pack, this design philosophy directly addresses it.
Sequential auto defrost system supports over 10 days of non-stop continuous mass production without a full shutdown. That is a real win for peak season when you can’t afford a 12-hour defrost window.
The honest limitation is vertical clearance. Plants with low ceilings or mezzanines can’t accommodate the spiral stack. Measure your building height before you spec this one.
For Whom This Pick Works
Plants with narrow ground area but sufficient vertical height will get the most out of the spiral path. Frozen vegetable and fruit processors will appreciate the low-dehydration gentle freezing mode. Peak-season operations will benefit from the long defrost interval.
Where It Stops Being the Right Answer
Plants with low ceilings can’t accommodate the vertical stack. For high-volume 3000+ kg/hr needs, the larger blast tunnel is a better fit.
Buying Guide: How to Choose the Right Spiral Freezer for Your Food Plant
The right spiral freezer is the one that matches your product geometry, throughput, sanitation cycle, refrigerant strategy, and 10-year total cost of ownership. Below is the decision framework I walk plant engineers through before they sign a purchase order. I’ve broken it into six concrete sections so you can skip to the part that matters for your operation.
Spiral vs Tunnel Freezer: When the Vertical Footprint Wins
A spiral freezer uses a helical belt conveyor stacked across 30 to 40 tiers inside an insulated enclosure, while a tunnel freezer uses a straight horizontal belt of fixed length. The vertical stacking is what gives spiral freezers their footprint advantage: a 10,000 lb/hr spiral typically fits in a 12 ft by 16 ft area where a tunnel needs 80 to 120 linear feet. If your plant floor is constrained, spiral wins on layout. If your ceiling height is constrained or you need a single-pass long residence time for a dense product, a horizontal tunnel can be simpler.
Capacity-wise, spirals scale from 1,000 lb/hr for small operations to 40,000 lb/hr for large export plants. Tunnels cap lower because belt length is the limiting factor. Hygienic access is similar between the two when both are designed to 3-A sanitary standards with CIP, but spirals add belt-tension monitoring as a maintenance task that tunnels don’t have. Capital cost per pound of capacity favors spirals at high volume; tunnels can be cheaper for low-volume, single-product plants.
Refrigerant Decision: Ammonia, CO2, HFC, or Cryogenic
Four refrigerant paths dominate the industrial freezer market today, and the AIM Act HFC phase-down has changed the math since 2024. Ammonia (R-717) is the workhorse for plants above 10,000 lb/hr because it has zero GWP, the best coefficient of performance, and the lowest operating cost per pound, but it triggers PSM compliance under OSHA 29 CFR 1910.119 at the 10,000 lb threshold and requires leak detection, ventilation, and emergency shutoff engineering.
CO2 (R-744) is gaining share in plants that want lower toxicity and simpler regulatory load. It has a GWP of 1 and performs well in cascade systems. HFCs like R-507 are still legal in 2026 but their GWP of 3,985 places them in the AIM Act phase-down bucket, and most plant engineers I work with are planning HFC-to-ammonia or HFC-to-CO2 retrofits within the next five years. Cryogenic LN2 and LCO2 have near-zero GWP and the fastest freeze times but the highest per-pound operating cost; they win on premium export SKUs and small-batch premium quality.
Capacity Sizing: Throughput Tier by Plant Size
The honest way to size a spiral freezer is to start with the upstream bottleneck (fryer discharge, blancher exit, forming line output) and then add 15 to 25 percent headroom for product mix variability and future SKU additions. A small artisan plant running one shift typically needs 500 to 2000 lb/hr, a mid-sized plant running two shifts needs 2000 to 8000 lb/hr, and a large export plant running 24/7 needs 8000 to 40,000 lb/hr.
Under-sizing is the most common capex regret I see. Operators consistently describe leaving capacity on the table because airflow parameters were not optimized post-installation. Air velocity, belt speed, and tier spacing need to be tuned to your specific product density and thermal load, not just left at factory defaults.
Sanitary Design and CIP Requirements
If your line runs USDA FSIS or FDA FSMA inspected product, sanitary design is non-negotiable. Look for 3-A sanitary standards, NSF certification, seamless TIG-welded stainless steel, sloped floors at 1/4 inch per foot toward drains, fin spacing of 3 to 4 fins per inch on evaporators, and CIP spray balls that hit every food-contact surface. Wash-down labor is one of the largest hidden operating costs in any freezer fleet.
Plants without proper hygienic design can face a 2x to 4x labor cost multiplier on sanitation. Allergen changeover time between products on a single line is another silent cost: a poorly designed line can take 90 minutes between an allergen run and a non-allergen run, while a properly designed CIP-ready line can do it in 20 to 30 minutes. Over a year, that adds up to dozens of recovered production hours.
Installation and Hidden Costs Most Buyers Miss
Forum operators and trade-press coverage consistently flag the same five hidden costs: PSM compliance engineering for ammonia systems, structural slab reinforcement for large spirals, glycol heat trace for freezer floors in cold climates, electrical service upgrades to handle compressor load, and integration engineering to dock the freezer with upstream and downstream conveyor lines. Budget 15 to 30 percent above the equipment quote for these items in a retrofit; budget 8 to 15 percent for a greenfield plant where the slab is already designed to spec.
Refrigerant transition is the emerging line item. If you are buying an HFC-based spiral in 2026, factor in the AIM Act phase-down cost over the next 5 to 10 years. The same dollar buys more capacity in an ammonia or CO2 system today, and the regulatory direction is clear.
TCO and ROI: What 10 Years Actually Costs
The honest 10-year TCO breakdown for a mid-sized plant looks like this: 30 to 40 percent capital cost (installed), 40 to 50 percent energy and refrigerant, 10 to 15 percent maintenance and parts, and 5 to 10 percent downtime. Downtime cost per hour varies by plant size and product mix, but a frozen pizza line running 8000 lb/hr can lose tens of thousands of dollars per hour in margin when the line is down, which makes predictive maintenance sensors a quiet but powerful ROI line item.
Cryogenic systems have lower capital cost per pound at small scale but the highest operating cost per pound, so they shine on premium SKUs and fade on commodity volume. Mechanical ammonia systems have the highest capital cost and the lowest operating cost per pound, so they win on long-run TCO at 10,000+ lb/hr scale. Hybrid systems that use a mechanical pre-cool and a cryogenic polish are gaining share for plants that need both throughput and texture.
Choosing by Food Category
The right spiral freezer for your plant depends heavily on what you actually freeze. Below is a quick category-by-category steer based on what I see working in real plants. If you also need help with smaller commercial equipment, the 10 Best Commercial Freezers for Restaurants guide covers the back-of-house scale, while this list focuses on industrial throughput.
Poultry processing lines need high throughput, hygienic CIP access, and belt systems that handle irregular product. The high-volume blast tunnel (pick #3) and the scalable modular unit (pick #9) are both strong fits. Industry data shows that belt speed tuning alone can recover 7 percent yield on a frozen poultry line.
Seafood IQF (shrimp, scallops, fish fillets) benefits from the mesh belt architecture (pick #5 or #6) for irregular shapes, the fluidized bed (pick #1) for small IQF separation, and the cryogenic unit (pick #2) for premium sashimi and export-grade texture. Pacific NW seafood processors have reported 12 to 15 percent reject reduction by switching from self-stacking to positive-drive belts.
Frozen pizza production needs long residence times and gentle handling. The vertical spiral extended path (pick #10) and the entry-level continuous unit (pick #7) both work, depending on volume tier.
IQF vegetables (peas, corn, broccoli, diced vegetables) are the fluidized bed’s natural fit (pick #1). The cryogenic unit (pick #2) wins on premium export vegetables where color retention matters more than throughput.
Frequently Asked Questions
What is a spiral freezer and how does it work?
A spiral freezer is a continuous industrial freezing system that uses a helical belt conveyor stacked across 30 to 40 tiers inside an insulated enclosure. Products enter at the base on a food-grade spiral belt, travel upward through progressively colder air zones driven by mechanical (NH3, CO2, HFC) or cryogenic (LN2, LCO2) refrigeration, and exit fully frozen at the discharge, typically at 1,000 to 40,000 lb/hr throughput depending on configuration.
What is the difference between a spiral freezer and a tunnel freezer?
A spiral freezer stacks a helical belt vertically to fit long residence times into a small footprint (typically 12 ft by 16 ft for a 10,000 lb/hr unit). A tunnel freezer runs a straight horizontal belt and needs 80 to 120 linear feet to deliver comparable capacity. Spiral wins on footprint and high-volume scalability; tunnel wins on simpler maintenance and lower ceiling-height requirements.
How long does a spiral freezer last?
A well-maintained spiral freezer typically delivers 15 to 25 years of service. Belt life is 5 to 10 years depending on product and tension, compressor life is 15 to 20 years with proper vibration monitoring, and the structural enclosure can run indefinitely with periodic insulation and seal replacement.
What refrigerant is best for spiral freezers in food plants?
Ammonia (R-717) is the workhorse for plants above 10,000 lb/hr thanks to zero GWP, the best coefficient of performance, and the lowest operating cost per pound. CO2 (R-744) is gaining share where lower toxicity matters. HFCs are in AIM Act phase-down. Cryogenic LN2 and LCO2 win on premium export SKUs.
How much does a spiral freezer cost?
Capital cost depends on capacity, belt type, and refrigerant. A small 1,000 lb/hr unit typically starts in the low six figures installed, while a high-volume 20,000 lb/hr ammonia spiral with full sanitary design runs into seven figures. Budget 15 to 30 percent above the equipment quote for installation, PSM compliance, and structural slab work in a retrofit.
Are ammonia freezers safe in food processing plants?
Yes, when engineered to OSHA 29 CFR 1910.119 PSM standards. Ammonia systems above 10,000 lb require leak detection, emergency shutoff, mechanical ventilation, and operator training. Properly engineered ammonia plants have decades of safe service. The trade-off is regulatory load versus the best thermodynamic performance and zero GWP.
Conclusion
Choosing the best spiral freezer for food plants in 2026 comes down to matching product geometry, throughput, refrigerant strategy, and 10-year total cost of ownership. The Industrial Fluidized Bed Tunnel Freezer is my editor’s choice pick for IQF separation on berries, peas, and small shrimp because the fluidized architecture delivers clean separation in 3 to 15 minutes with hygienic CIP-ready construction. For premium export SKUs that need -196°C flash freeze, the cryogenic liquid nitrogen unit is the right answer. For high-volume commodity lines running 3000 kg/hr or more, the continuous blast tunnel with dual pre-cool and deep-freeze zones is the workhorse pick.
Before you sign a purchase order, walk your operations team through the six-step decision framework in the buying guide: spiral vs tunnel, refrigerant choice, capacity sizing, sanitary design, installation hidden costs, and 10-year TCO. Get those six decisions right and the rest of the project runs smoother. If you’re also scaling your cold chain with smaller units, check out our 10 Best Chest Freezers for Garages review for the back-of-house scale.