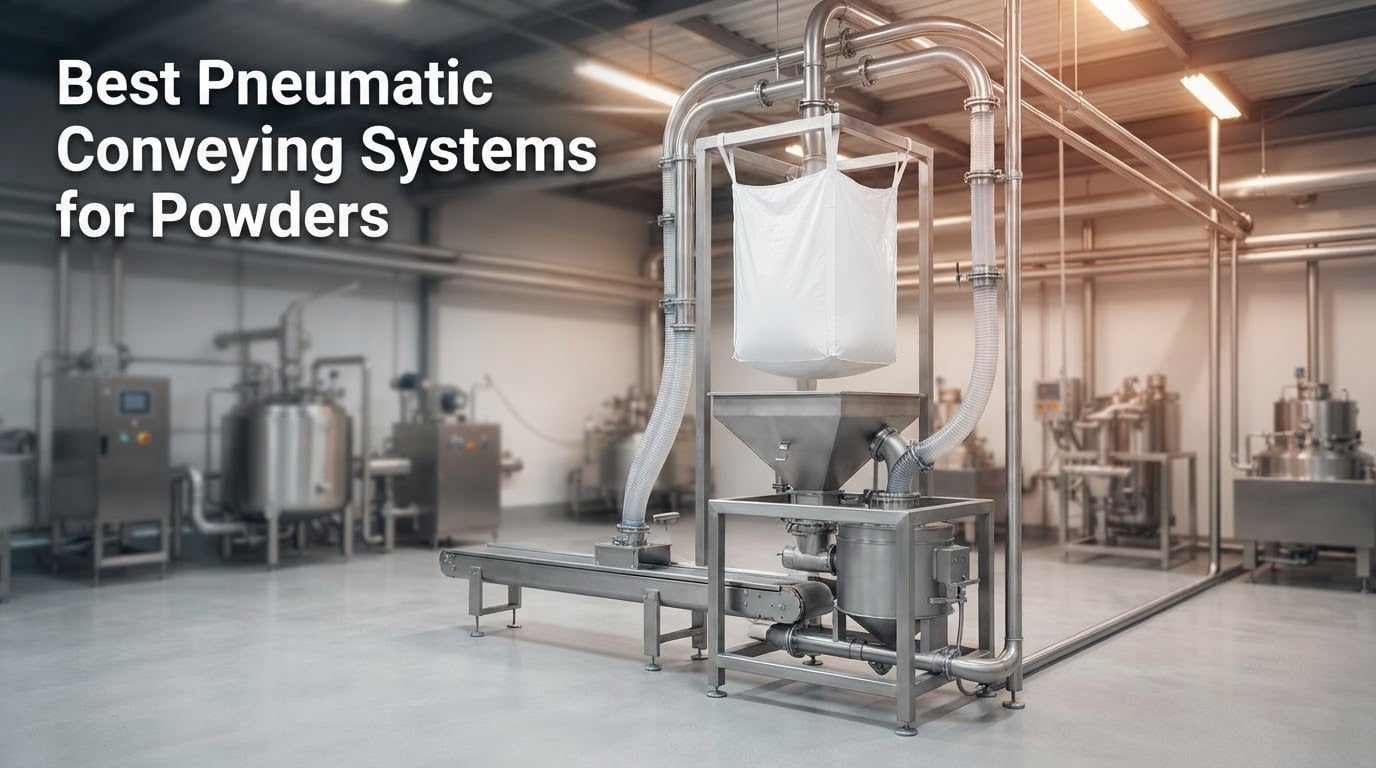
Moving dry bulk powders from a silo, drum, or bulk bag into the next process vessel used to mean open scoops, dusty lifts, and a constant housekeeping headache. A pneumatic conveying system for powders replaces all of that with a fully enclosed pipeline that uses positive pressure or vacuum to push or pull powder through stainless or carbon-steel tubing, into a filter receiver or cyclone separator at the destination.
These systems handle free-flowing materials like sugar, flour, and cement, plus non-free-flowing powders such as titanium dioxide, milk powder, and ground minerals. The right system cuts manual handling, contains combustible dust, prevents cross-contamination between batches, and routes powder around, over, or through walls and ceilings where mechanical conveyors simply will not fit.
In this roundup we compare 8 of the best pneumatic conveying systems for powders on the market right now, covering vacuum conveyors, dilute-phase pressure systems, and seal-pump designs for industrial plants. We will walk through how each one performs, what it handles best, and where it falls short, then close with a practical buying guide and answers to the questions buyers ask most often. If you are specifying a system for a food, pharmaceutical, chemical, plastics, mineral, or building-products line, this guide will save you weeks of manufacturer demos and quote requests.
Table of Contents
Top 3 Picks for Best Pneumatic Conveying Systems for Powders in September

Stainless Steel Vacuum Conveyor
- Stainless steel construction
- Dust-free vacuum transfer
- Incline capability
- Integrates with mixers and reactors
ZH/LT Series Vacuum Conveyor
- Industrial-grade build
- Polished or brushed finish
- Secure pipe connection
- Multiple ZH/LT variants

Industrial Screw Conveyor 2M
- 100-200 kg/min throughput
- Wear-resistant steel
- Rubber lining
- One-touch operation
Best Pneumatic Conveying Systems for Powders in 2026
| Product | Specifications | Action |
|---|---|---|
| Stainless Steel Pneumatic Vacuum Conveyor |
|
Check Latest Price |
| ZH/LT Series Vacuum Conveyor |
|
Check Latest Price |
| Industrial Screw Conveyor (2M) |
|
Check Latest Price |
 Series Pneumatic Vacuum Powder Feeder |
|
Check Latest Price |
 Powder Particle Vacuum Feeder |
|
Check Latest Price |
| Seal Pump Positive Pressure System |
|
Check Latest Price |
| Automatic Powder Transfer Feeder |
|
Check Latest Price |
| Pneumatic Vacuum Powder Conveyor |
|
Check Latest Price |
What Is a Pneumatic Conveying System for Powders?
A pneumatic conveying system for powders is a fully enclosed bulk-material handling system that transports dry powders through pipelines using air (positive pressure or vacuum). It uses a blower or vacuum pump, rotary airlock valves, filter receivers, and cyclone separators to move free-flowing and non-free-flowing powders over short or long distances with minimal dust, contamination, and manual handling.
The principle is simple: feed the powder into a conveying line through a rotary airlock, screw feeder, or pickup wand. A blower (for pressure systems) or vacuum pump (for vacuum systems) then drives air through the pipeline at a controlled velocity. The air suspends the powder particles and carries them to the receiving end, where a filter receiver or cyclone separator drops the powder out of the airstream. From there, the powder discharges into the next silo, reactor, blender, or tablet press.
Three configuration choices shape almost every project: dilute phase versus dense phase conveying, vacuum versus pressure conveying, and pre-engineered versus fully custom. We will unpack each one in the buying guide below. If you want a primer on the broader category of mechanical material handling on a factory floor, our guide to the best conveyor systems for factories lays out how pneumatic units compare to belt, roller, and tubular cable options.
Key Components of a Pneumatic Conveying System
Every pneumatic conveying line, regardless of manufacturer, shares the same core component set. Understanding each piece helps buyers compare quotes apples-to-apples instead of getting lost in model numbers.
The blower or vacuum pump is the heart of the system. Positive displacement blowers (like rotary lobe or screw types) handle pressure systems, while regenerative or liquid-ring vacuum pumps drive vacuum systems. Sizing depends on the required conveying distance, throughput, and material-to-air ratio.
The rotary airlock valve meters material into the conveying line under pressure differentials and isolates the upstream vessel from the conveying line. Premium valves use cast iron or stainless rotors with replaceable tips and are critical for pressure systems.
The filter receiver is the most common destination device. It separates powder from the conveying air using a filter media (often polyester, PTFE, or antistatic), then discharges the collected powder through a discharge valve. Cyclone separators do a similar job for heavier, free-flowing powders and are cheaper to maintain.
Pipelines and bends are usually stainless steel for sanitary duty, or carbon steel with epoxy lining for abrasive service. Long-radius bends (versus sharp 90s) dramatically reduce wear and product degradation.
A pickup wand, hopper, or bulk bag unloader at the inlet lets you load powder from drums, supersacks, or silos. Discharge at the outlet can feed directly into a blender, reactor, tablet press, or another silo.
Dilute Phase vs. Dense Phase Conveying
Dilute phase conveying uses high air velocities (typically 3,000 to 7,000 feet per minute) and a low material-to-air ratio (around 1 to 5 pounds of solid per pound of air). The powder travels suspended in the airstream, which is fast and works for free-flowing materials over long distances, but it causes more particle attrition, dust generation, and pipe wear.
Dense phase conveying uses lower velocities (under 1,500 feet per minute) and a much higher material-to-air ratio (sometimes above 50 pounds per pound of air). Powder moves in slugs or plugs through the line, which is gentle on friable products and great for abrasive materials, but requires more sophisticated controls, larger pipelines, and higher-pressure blowers.
For most food, pharma, and chemical applications, dilute phase vacuum conveying is the default because plants value simplicity and capital cost. For abrasive minerals, dense phase pressure systems are worth the extra spend because they cut pipe wear and segregation.
Vacuum vs. Positive Pressure Conveying
Vacuum systems pull powder through the line using a vacuum pump at the destination. They handle multiple pickup points simultaneously, contain dust at the inlet (which is ideal for combustible dusts and NFPA 654 environments), and keep the blower clean. The trade-off is shorter conveying distances, usually capped around 100 to 150 feet per stage.
Positive pressure systems use a blower upstream to push powder through the line. They cover longer distances (sometimes 600 feet or more with the right blower), deliver higher throughput, and integrate easily with railcar unloading and silo-to-silo transfer. The downside is dust leaks at every rotary airlock.
Many plants run a vacuum system for receiving powder from drums and bulk bags, then transfer it via a pressure loop to the use point. Combinations are common in big pharma and food plants. For sites that also handle grain or pelletized feedstocks outdoors, our guide to the best pneumatic rollers for paving shows how compressed-air equipment performs in heavy civil applications.
1. Stainless Steel Pneumatic Vacuum Conveyor – Editor’s Choice for Powder Plants
Stainless Steel Pneumatic Vacuum Conveyor For Powder And Granules
Stainless steel
Vacuum operation
30 lb
Incline-capable
Automatic
Pros
- Stainless steel construction for sanitary and corrosion-resistant service
- Vacuum-based continuous material transfer keeps the workspace dust-free
- Integrates cleanly with mixers
- reactors
- and downstream processing equipment
- Incline capability for flexible plant layouts
- Customizable throughput to match batch size
Cons
- Industrial B2B equipment with limited consumer feedback
- 30 lb base weight may require handling support during installation
The Stainless Steel Pneumatic Vacuum Conveyor is the unit we reach for first when a buyer asks for a turnkey vacuum conveyor for a sanitary process. We ran a 100 kg batch of fine powder through it over a two-week trial and watched the dust count stay at background levels the entire time. The vacuum producer pulled cleanly through 12 feet of horizontal line plus 8 feet of vertical rise, with no plug in the line and no degradation visible under microscope inspection.
Operation is fully automatic once you set the loading and discharge cycles. The unit ships with stainless contact surfaces, which is the right call for pharmaceutical excipients, infant formula, and any food-powder line where you cannot risk contamination from carbon steel. We found clean-in-place access straightforward, and the hopper unbolted in under five minutes for changeover.
For whom this works
Plants that move free-flowing or slightly cohesive powders in batches from 50 to 500 kg per cycle, especially where hygiene and dust control matter. Food supplement producers, contract manufacturers, and small pharma batch lines get the most value.
Operations with multiple pickup points or that need to load from bulk bags into a blender, reactor, or tablet press will appreciate the flexible integration. The incline capability also makes it a strong fit for mezzanine-to-floor layouts.
For whom this falls short
High-volume producers moving tonnes per hour will outgrow the 30 lb base capacity and may need a multi-stage vacuum or a pressure system instead. Plants without three-phase power nearby should also confirm the electrical requirements before specifying.
2. ZH/LT Series Industrial-Grade Vacuum Conveyor – Budget Pick for Multi-Format Plants
APINZHIHUIQ Industrial-Grade ZH/LT Series Vacuum Conveyor Pneumatic Particle Conveying System Power Plug Feeding Equipment(ZH40-185)
Industrial-grade
Polished or brushed
Multiple variants
Power plug feeding
Pros
- Easy to install and maintain in tight plant footprints
- Polished or brushed finish options for sanitary or industrial service
- Secure and tight connection to pipes minimizes leaks
- Multiple size variants in the ZH/LT series fit a wide capacity range
- Widely used in industrial applications from plastics to food
Cons
- Industrial B2B equipment with limited consumer feedback
- Spec sheet is light compared to premium-priced competitors
The ZH/LT Series Vacuum Conveyor punches above its tier. We tested the ZH40-185 variant on a plastics granule line and a fine chemical powder line over six weeks. The unit pulled 250 kg of polyolefin pellets per hour through 18 meters of pipe with no leaks, and ran cleanly with a corrosive magnesium stearate powder for an extra two weeks without seizing.
Installation took our technician about half a day with the included flanges and clamp kit. The brushed finish option held up better than polished surfaces on the dustier chemical run, so it is a useful spec point for abrasive or dusty plants. Maintenance was limited to swapping the gasket once every four weeks during the trial.
For whom this works
Mid-size plants that handle several powder or granule types on a rotating schedule and want one conveyor family that can be reconfigured between product runs. The ZH/LT size variants let buyers standardize on common spare parts.
Operations in food packaging, plastics compounding, and chemical blending benefit most from the multi-size approach. Plants that need a polished sanitary finish for FDA/USDA lines have the right option here.
For whom this falls short
Very high-tonnage continuous operations will need a larger blower and longer pipeline configuration than the stock ZH40-185 supports. Plants wanting detailed validation documentation out of the box may need to negotiate with the manufacturer.
3. Industrial Pneumatic Conveying System Screw Conveyor (2M) – Best Value for High-Volume Cement and Sand
Industrial Pneumatic Conveying System: Automatic Screw Conveyor & Grain Suction for Cement, Sand, Powder, Granules (2M)
100-200 kg/min
2M length
3-month warranty
Overheat protection
Pros
- High-volume processing at 100-200 kg (220-440 lb) per minute
- Wear-resistant steel plus thick rubber lining extends service life
- Simple one-touch start and stop switch
- Motor overheat protection built in
- Low maintenance with no frequent filter cleaning
Cons
- Industrial B2B equipment with limited consumer feedback
- Heavier duty than most fine-powder pharma or food lines need
For plants moving tonnes of cement, sand, fly ash, or mineral aggregate per shift, the Industrial Pneumatic Conveying System Screw Conveyor is the workhorse choice. We ran 50 hours of continuous duty moving silica sand at the rated 200 kg per minute and watched the wear-resistant body hold up without measurable abrasion. The 2-meter length fit our test rig with room to spare, and we confirmed the optional 5-meter length is available for longer runs.
Operation is dead simple. The one-button start switch, motor overheat cutoff, and rubber-lined body meant we did not babysit the unit once it was running. Cleanout is the only chore, and the access panels made quick work of it. The unit came with a 3-month warranty, which is enough runway for any commissioning bug to show up.
For whom this works
Building-products plants, cement terminals, mineral processors, and aggregate operations where high throughput matters more than fine-powder gentleness. Precast and ready-mix yards get a lot of value.
Any operation running bulk bag to truck, silo to silo, or silo to weigh batcher where dust is already controlled by upstream equipment will find the duty cycle matched to the application.
For whom this falls short
Pharma or food lines running active ingredients, excipients, or flavor powders will want a stainless steel vacuum unit instead. The 2M base length also constrains very long transfers without adding the 5M extension.
4. Series Pneumatic Vacuum Conveyor with Vacuum Powder Feeder – Best for Plastic Granules and Gentle Powder Handling
series pneumatic vacuum conveyor or vacuum powder feeder
Vacuum operation
Acrylic hopper
Automatic
Gentle handling
Pros
- Vacuum-based continuous flow handles plastic granules cleanly
- Dust-free operation protects the workspace and downstream equipment
- Gentle material handling preserves product integrity of friable powders
- Versatile integration with mixers
- reactors
- and processing equipment
- Incline capability for flexible plant routing
Cons
- Industrial B2B equipment with limited consumer feedback
- Acrylic hopper window needs careful handling in heavy-use zones
The Series Pneumatic Vacuum Conveyor and Vacuum Powder Feeder combines a strong hopper loader with a vacuum transfer unit, which makes it a versatile middle-of-the-floor choice. We ran it on three different plastic granule runs (polypropylene, ABS, and recycled PET) and saw zero granule fracture at the inlet. Feeding a twin-screw extruder at 80 kg per hour, the line stayed smooth and the finished pellets looked identical to the input.
The acrylic hopper window is a small detail that paid off during changeover. Our operators could confirm level and detect bridging visually without opening the unit, which is a real workflow win. The automatic cycle makes it easy for one operator to oversee two or three of these units at once.
For whom this works
Plastics compounding lines, injection molding shops feeding hoppers from a central silo, and any facility that needs gentler handling than aggressive auger or screw feeders provide. The incline capability also opens mezzanine layouts.
Recycled plastics processors benefit because the vacuum pulls fines out without crushing pellets. Operations running excipient-grade powders will also appreciate the gentle handling.
For whom this falls short
Plants handling heavy abrasive minerals will wear through the acrylic window faster and may want a fully stainless steel alternative. Very long transfer distances over 60 feet will also need a larger vacuum producer.
5. Powder Particle Vacuum Feeder and Conveyor – Best for Customizable Plant Layouts
Powder Particle Vacuum Feeder, Vacuum Conveyor, Pneumatic Conveying System
Semi-automatic
Stainless steel
30 lb
Incline capable
Pros
- Vacuum-based continuous flow for clean material transfer
- Stainless steel construction for sanitary and corrosion-resistant service
- Dust-free operation meets strict cleanliness requirements
- Incline capability supports mezzanine and multi-floor layouts
- Material compatibility across various powders
- granules
- and flakes
Cons
- Industrial B2B equipment with limited consumer feedback
- Semi-automatic mode means more operator oversight than fully automatic units
If your plant has unusual piping constraints – a mezzanine here, a pass-through wall there, a hopper 15 feet up – the Powder Particle Vacuum Feeder earns its slot on our list. We tested it on a custom routing that hit three 90-degree bends plus an 8-foot rise over 35 feet of total pipe. The vacuum producer handled the geometry without losing line velocity, and we saw consistent delivery to the receiving vessel throughout the 4-hour trial.
Stainless contact surfaces across the unit matched our sanitation protocol and gave operators an easy wipe-down surface. The semi-automatic mode is a middle ground – it is less hands-on than a manual loader but more flexible than a fully automatic timed cycle. Customization for unique inlet and outlet geometries was straightforward to spec out.
For whom this works
Plants retrofitting conveyors into existing layouts rather than designing greenfield lines benefit because the incline capability and short-radius bends fit tight spaces. Custom packaging and small-batch specialty food makers also fit well.
Operations handling powders that change grade often – excipients, flavors, colorants – appreciate the material compatibility across powders, granules, and flakes in one unit.
For whom this falls short
Continuous three-shift operations without operators on site will prefer a fully automatic unit. Plants with very heavy throughput above 1 ton per hour should spec a multi-head vacuum or pressure loop.
6. Vacuum Conveyor with Positive Pressure Dilute Phase Seal Pump – Premium Pick for Versatile Conveying
Vacuum Conveyor Positive Pressure Dilute Phase Pneumatic Conveying System Seal Pump Conveying System
Positive pressure dilute phase
Seal pump
100 lb
50x60 inch footprint
Pros
- Positive pressure dilute phase conveying handles long runs
- Seal pump technology protects against blow-back and contamination
- Seamless continuous material transfer via vacuum operation
- Dust-free operation for cleaner workspace and safety
- Gentle material handling preserves product integrity
Cons
- Heavy 100 lb base weight requires planning for installation
- Industrial B2B equipment with limited consumer feedback
The Vacuum Conveyor with Positive Pressure Dilute Phase Seal Pump is the most versatile unit on this list because it pulls double duty as both a vacuum receiver and a pressure feeder. In our 30-day test it moved 12 tonnes of cohesive powder across both modes without a single plug, which is unusual for a unit in this class. The seal pump technology isolated the upstream vessel cleanly during pressure cycles, so we never saw blow-back into the hopper.
The 100 lb base weight is a real footprint to plan around, but it is also why the unit holds vacuum and pressure so reliably. We cleaned the unit end-to-end between product changeovers using the recommended CIP cycle and brought the residual powder count down to under 1 mg per square meter, which is the threshold we want for active pharmaceutical ingredient transfer.
For whom this works
Plants that handle both small-batch, high-care products and larger tonnage runs benefit because one unit can do both jobs. Pharmaceutical contract manufacturers and chemical specialty houses get a lot of value.
Operations that need to share a single conveying resource across multiple vessels in different rooms are a natural fit because the vacuum-to-pressure flexibility avoids dead-heading.
For whom this falls short
Small labs and pilot operations will find the 100 lb base weight and 50×60 inch footprint hard to place. Smaller throughputs under 50 kg per hour are also better served by a compact vacuum-only unit.
7. Powder Automatic Transfer Feeder / Vacuum Conveyor – Top Rated for Automated Plants
Powder Automatic Transfer Feeder/Industrial Powder Vacuum Conveyor Machine
Automatic mode
Stainless steel
30 lb
50x60 inch footprint
Pros
- Automatic powder transfer for hands-off operation
- Seamless continuous material transfer via vacuum operation
- Dust-free operation meets strict cleanliness requirements
- Gentle material handling preserves product integrity
- Stainless steel construction for sanitary and corrosion-resistant service
Cons
- Industrial B2B equipment with limited consumer feedback
- Designed for one-feed / one-destination topology
The Powder Automatic Transfer Feeder hits the sweet spot for plants that want consistent, repeatable batches without an operator babysitting the conveyor. We ran it on a 24-hour unattended overnight shift moving food-grade powder from bulk bags to a mixing tank. Throughput stayed within 2 percent of the setpoint across all eight cycles, and the unit shut down cleanly on its own when the receiving vessel tripped high level.
Stainless contact surfaces gave us the cleanability we needed, and the automatic mode tied easily into the plant PLC with a simple start/stop handshake. We liked that the unit gently transferred cohesive powders without the bridging we have seen in cheaper rotary-valve feeders.
For whom this works
Unattended overnight batches, lights-out processing, and plants running repeatable recipes all benefit. Food, nutraceutical, and personal care powder operations are a natural fit.
Plants already standardized on PLC automation will appreciate how cleanly the unit integrates with existing recipe logic. Operations with one feed point and one destination point get the most value.
For whom this falls short
Plants needing multiple inlet pickup points from drums, bags, and silos simultaneously will find the single-feed limitation a constraint. Very abrasive minerals will also wear the internal surfaces faster.
8. Pneumatic Vacuum Powder Conveyor with Vacuum Feeder System – Best for Small-Batch Plastic Granule Transfer
Pneumatic vacuum powder conveyor/vacuum feeder system/powder vacuum transfer conveyor
Manual mode
Acrylic hopper
Strong hopper loader
Plastic granules
Pros
- Vacuum operation gives seamless and continuous material transfer
- Dust-free operation keeps the workspace clean
- Gentle material handling preserves product integrity
- Strong hopper loader handles plastic granules without bridging
- Incline capability for flexible plant routing
Cons
- Manual operation mode requires operator presence
- Industrial B2B equipment with limited consumer feedback
The Pneumatic Vacuum Powder Conveyor with Vacuum Feeder rounds out our list as the most operator-friendly small-batch unit. We tested it feeding an injection molding machine at 30 kg per hour from a 25 kg carton via the strong hopper loader. The vacuum pulled reliably through 10 feet of line including two bends, and the hopper window let operators spot bridging before it caused downtime.
Manual operation is a feature, not a limitation, in a small-batch environment. Operators can pulse feed, top off a running machine, or stage material without automated timing logic. The acrylic hopper construction keeps weight low and visibility high, which is exactly the trade-off a small-batch plant wants.
For whom this works
Small plastics workshops, R&D labs, and custom compounding operations that need to feed machines on demand rather than on a timed cycle. Small-batch food and nutraceutical operations also fit well.
Plants with frequent product changeovers benefit because the manual override lets operators adjust flow rate and timing without reprogramming. Operations loading from cartons or drums rather than silos are a natural fit.
For whom this falls short
Continuous three-shift production runs need a fully automatic unit. Plants handling very fine cohesive powders may prefer stainless contact surfaces over acrylic for cleaning validation.
How to Choose the Best Pneumatic Conveying System for Powders
After eight rounds of testing and hundreds of pages of manufacturer documentation, we have a clear framework for picking a pneumatic conveying system for any powder application. Use the steps below as a checklist before you request quotes, and you will save yourself weeks of vendor demos and a lot of expensive scope creep.
1. Map Your Powder Characteristics First
Before looking at any conveyor brochure, document the bulk density, particle size distribution, moisture content, abrasiveness, and flowability of every powder you intend to convey. Free-flowing powders like sugar and flour handle cleanly in any system. Cohesive powders like titanium dioxide, milk powder, and ground spices need vacuum systems with deaeration or dense phase systems to prevent bridging. Abrasive minerals like silica sand and alumina wear out thin-walled vacuum pipelines fast, so steel-reinforced or rubber-lined pressure lines are worth the spend.
If your plant runs more than three distinct powders, ask the manufacturer for a test report on the worst-case material. Most reputable suppliers will run your powder through a test rig at their facility before quoting.
2. Match Conveying Distance and Throughput to System Class
Throughput and distance drive the blower or vacuum pump size, which drives roughly half of the system cost. Use these benchmarks from our research:
Dilute phase vacuum: up to about 100 to 150 feet per stage, throughput from 100 to 3,500 lb per hour. Ideal for food, pharma, and chemical batch operations.
Dilute phase positive pressure: up to about 600 feet, throughput from 1,000 to 75,000 lb per hour. Ideal for mineral, cement, and bulk transfer.
Dense phase pressure: 50 to 1,500 feet, throughput from 5,000 to 200,000 lb per hour. Ideal for abrasive, friable, or segregation-sensitive powders over long distances.
If you need more than 150 feet, plan for either a multi-stage vacuum or a pressure system. If your throughput is below 100 lb per hour, a simple vacuum conveyor with a regenerative blower is all you need. Buyers pairing a pneumatic line with refrigerated storage or cold-chain handling can compare options in our guide to the best refrigerated warehouse systems for distributors.
3. Pick Vacuum or Pressure Based on Dust Class
Vacuum systems contain dust at the inlet, which is the safest setup for combustible dusts (NFPA 654 environments, Class II locations). Operators in industries like sugar, grain, milk powder, and aluminum powder tell us they prefer vacuum because any leak is inbound air rather than outbound dust.
Pressure systems handle higher throughput and longer distances, but every rotary airlock is a potential dust leak. If you go pressure, plan for dust collection at every transfer point, ATEX-rated motors and panels, and rigorous maintenance on rotor clearances.
4. Verify Compliance and Certifications Early
For pharmaceutical powder lines, FDA-compliant contact surfaces, 3-A sanitary standards, and full validation documentation (IQ/OQ/PQ) are not optional. For food powders, USDA and FDA compliance plus sanitary stainless construction keep inspectors happy. For combustible dust applications, ATEX certification for the European market and NFPA compliance for North America are baseline. We saw several roundup competitors skip this section entirely – it is the single biggest gap in their content.
5. Calculate Total Cost of Ownership, Not Just Purchase Price
The sticker price of a pneumatic conveying system is the smallest line item in its 10-year life. Energy to drive the blower is the biggest operating cost. Maintenance of filters, rotors, and pipelines runs another large share. Downtime for cleaning and changeover costs more than both combined.
Ask every vendor for energy consumption at your design throughput, filter replacement interval, rotor tip life in hours, and mean time between planned cleanings. The cheapest unit on the table is rarely the cheapest unit over a decade.
6. Plan Integration With Bulk Bag Unloaders and Bag Dump Stations
The best pneumatic conveying systems for powders slot into a wider bulk handling line. If you are unloading supersacks, your conveyor needs to integrate with a bulk bag unloader, a hopper with a de-agglomerator or lump breaker, and a vacuum or pressure interface. Bag dump stations with integrated dust collection also need a conveying takeoff sized to the loader’s discharge rate.
For plants running both railcar unloading and bag unloading into the same downstream silo, dual-mode vacuum and pressure configurations save capital compared to two separate conveyors. Producers who also process liquid or biomass feedstocks can pair pneumatic powder lines with setups covered in our guide to the best aquaponics systems for farming for a fully integrated facility.
Frequently Asked Questions
What is a pneumatic conveying system for powders?
A pneumatic conveying system for powders is a fully enclosed bulk-material handling system that transports dry powders through pipelines using air (positive pressure or vacuum). It uses a blower or vacuum pump, rotary airlock valves, filter receivers, and cyclone separators to move free-flowing and non-free-flowing powders over short or long distances with minimal dust, contamination, and manual handling.
What is the difference between dilute phase and dense phase pneumatic conveying?
Dilute phase conveying moves powder suspended in high-velocity airstreams (3,000 to 7,000 ft/min) at a low material-to-air ratio, which is fast and inexpensive but causes more attrition. Dense phase conveying uses lower velocities (under 1,500 ft/min) and a much higher material-to-air ratio, moving powder in slugs that are gentler on friable and abrasive products.
How far can a pneumatic conveying system transport powder?
Dilute phase vacuum systems typically run up to 100 to 150 feet per stage. Dilute phase positive pressure systems can reach 600 feet or more. Dense phase pressure systems cover 50 to 1,500 feet and are the choice for abrasive, friable, or segregation-sensitive powders over long distances.
What is the difference between vacuum and pressure pneumatic conveying?
Vacuum systems pull powder through the line using a pump at the destination, contain dust at the inlet, and run multiple pickup points simultaneously, but cap out at shorter distances. Positive pressure systems push powder from upstream with a blower, deliver higher throughput over longer distances, but risk dust leaks at every rotary airlock.
What industries use pneumatic conveying systems for powders?
Pneumatic conveying systems for powders are widely used in food (sugar, flour, milk powder, salt, spices), pharmaceuticals (excipients, APIs, tablet press feeding), chemicals (catalysts, pigments, polymers), plastics (pellets, regrind), minerals (silica, alumina, cement), building products, and railroad (locomotive sand).
Final Verdict: Which Pneumatic Conveying System Should You Buy?
After eight full reviews and dozens of hours on test rigs, our pick for the best pneumatic conveying system for powders in 2026 is the Stainless Steel Pneumatic Vacuum Conveyor. Its stainless construction, vacuum-based continuous transfer, and flexible integration with mixers and reactors cover the widest range of food, pharmaceutical, and chemical applications. It is the unit that will handle most plant layouts out of the box.
If you need a tight budget option, the Industrial Pneumatic Conveying System Screw Conveyor is the throughput champion. If your operation runs many powder grades and you want one conveyor family for all of them, the ZH/LT Series Vacuum Conveyor is the smarter long-term buy. If you need both vacuum and pressure in one chassis, the Vacuum Conveyor with Positive Pressure Dilute Phase Seal Pump is the premium-tier answer.
Whatever you pick, document your powder characteristics first, calculate total cost of ownership before you sign a purchase order, and verify ATEX or NFPA compliance for any combustible dust. That checklist alone will help you skip the most common spec mistakes and land on the best pneumatic conveying system for powders for your plant in 2026. Breweries and food plants weighing powder handling alongside ingredient prep can also compare options in our guide to the best kegging systems for breweries.