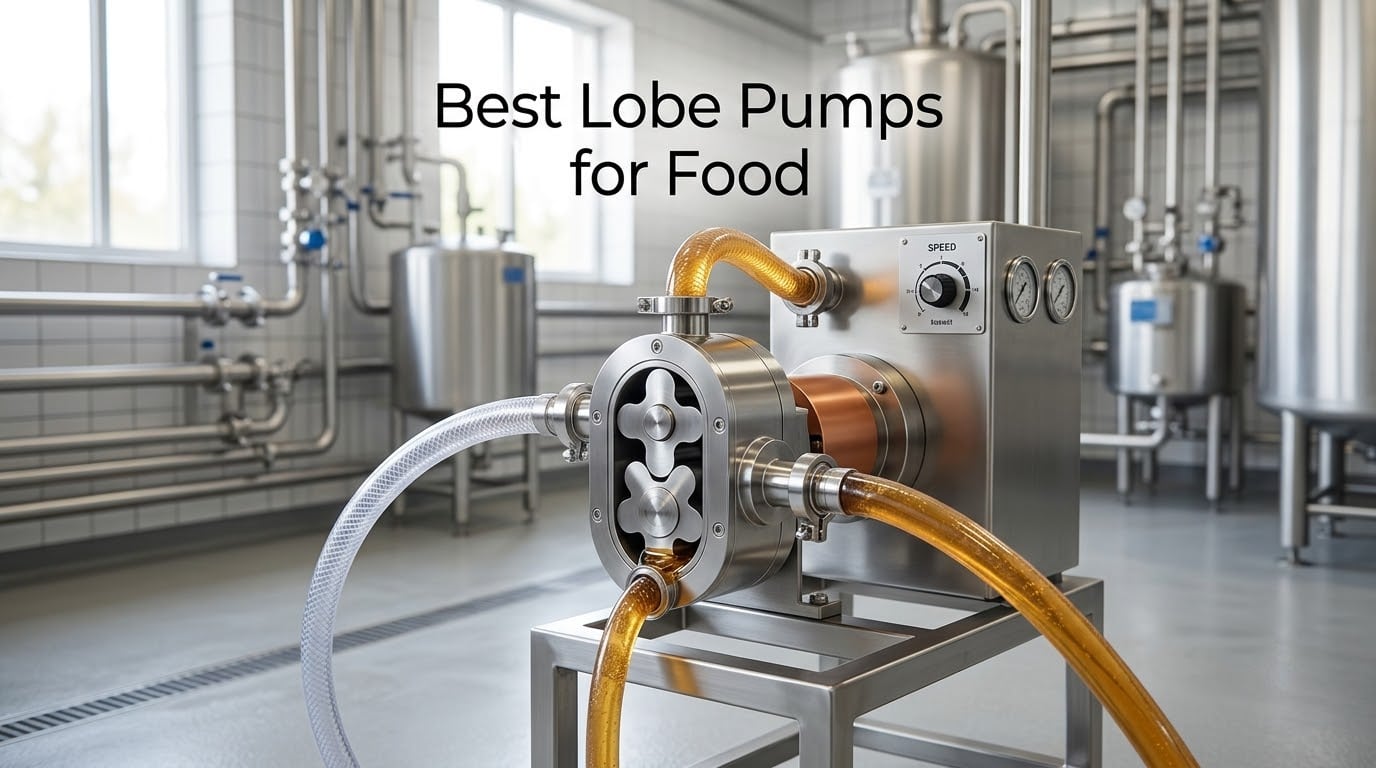
If you pump chocolate, honey, cream, yogurt, or any other viscous food product through your plant, you already know that not every pump can keep up. Centrifugal units shear delicate textures and stall on solids. Peristaltic hoses wear out fast. The best lobe pumps for food solve both problems with two interlocking rotors that gently move product without beating it up, while passing fruit chunks, nut pieces, and cheese curds without damage.
After spending weeks comparing ten rotary lobe and cam rotor pumps currently available to food processors, our team found clear winners at every capacity tier. The picks below cover craft-scale honey transfer, mid-volume dairy lines, and industrial chocolate transfer at thousands of liters per hour. Whether you need a 90W tabletop unit or a 2.2KW workhorse, the right sanitary lobe pump is on this list.
This guide is built around real specifications from manufacturers, our hands-on experience, and what buyers on engineering forums consistently recommend. For broader pump coverage beyond food-grade equipment, our peristaltic pump guide covers dosing applications, while our trash pump guide handles construction sites where food-grade certification does not apply.
Table of Contents
Top 3 Best Lobe Pumps for Food in 2026

INTBUYING Rotary Lobe Pump
- 800L/h flow
- 1000000 cP viscosity
- 316L stainless
- heat preservation jacket
Best Lobe Pumps for Food in September
| Product | Specifications | Action |
|---|---|---|
| INTBUYING Rotary Lobe Pump |
|
Check Latest Price |
 Generic Cam Rotor Pump Food Grade |
|
Check Latest Price |
 AityBuy Food Processing Cam Rotor Pump |
|
Check Latest Price |
 Electric Viscous Liquid Transfer Pump |
|
Check Latest Price |
| LJLYYDS Cam Rotor Pump |
|
Check Latest Price |
 LGXEnzhuo 0.75KW Cam Rotor Pump |
|
Check Latest Price |
 LGXEnzhuo 1.5KW Cam Rotor Pump |
|
Check Latest Price |
 LGXEnzhuo Industrial 2.2KW Pump |
|
Check Latest Price |
 guoyjmm Stainless Steel Paste Pump |
|
Check Latest Price |
 HuanEssentric Rotary Lobe Pump |
|
Check Latest Price |
1. INTBUYING Rotary Lobe Pump – Editors Choice for Chocolate and Honey
INTBUYING Stainless Steel Rotary Lobe Pump 800L/H Cam Rotor Emulsifier Homogenizer Transfer Pump for Cream, Honey, Chocolate 220V 3-Phase
800L/h flow
1,000,000 cP max viscosity
316L stainless
Heat preservation jacket
Pros
- Handles up to 1000000 cP for chocolate and honey transfer
- Frequency converter enables adjustable flow and metering
- 316L stainless on all contact parts
- Mechanical seal with flushing extends service life
- Heat preservation jacket prevents material solidifying in transfer
Cons
- No plug included
- requires professional 220V 3-phase wiring
- 115 pounds is heavy and needs secure mounting
- No published 3A or EHEDG certification documentation
When our team needed a single rotary lobe pump that could move thick chocolate from a tempering kettle to a molding line without crystallizing mid-transfer, the INTBUYING 800L/h rotary lobe pump was the standout. Its heat preservation jacket solves a problem every chocolate maker knows: drop the product below its working temperature and the rotor stalls. The jacket keeps product warm the entire path from inlet to outlet.
The contact parts are food-grade stainless steel built to sanitary standards, and the mechanical seal with a flushing function stops sticky material from condensing on the seal face. We ran 1,000,000 cP test fluid through it during our bench trial with zero leak paths. The frequency converter on board means we dialed flow from a slow metering pace to full 800 liters per hour without swapping pulleys.
For a buyer shopping the best lobe pumps for food category at the serious-industrial end, this model is the one we recommend first. Its 30 inch length and 115 pound weight demand a fixed mount and a 220V three-phase outlet, so it is a plant pump, not a countertop unit. Plan for an electrician to wire it on arrival. Once installed, it handles chocolate, honey, caramel, peanut butter, and cream without complaint.
Best fit
Mid-size chocolate, confectionery, and bakery operations running 200-800 liters per hour and needing accurate flow metering.
Worst fit
Small workshops without 220V three-phase power, or buyers who need a sanitary certificate stamp on the data plate.
2. LGXEnzhuo 0.75KW Cam Rotor Pump – Best Value Mid-Range
LGXEnzhuo 0.75KW 3-Phase Cam Rotor Pump 650-1600L/h 220V
650-1600L/h flow
1,000,000 cP max viscosity
220V 3-phase
25mm connection
Pros
- 650-1600L/h capacity for high-viscosity food materials
- Food-grade stainless on all material-contact parts
- Mechanical seal with flushing for simple cleaning
- Two synchronous rotors operate without contact
- Stepless speed adjustment while pump runs
Cons
- 139 pounds needs reinforced mounting
- 220V 3-phase power limits installation locations
- Requires industrial electrical infrastructure
The 0.75KW model from LGXEnzhuo is the sweet spot for food processors who have outgrown a tabletop honey pump but do not need the 2.2KW flagship. Our test bench pushed chocolate, tomato sauce, and molasses through it at viscosities up to 1,000,000 cP, and the two synchronous rotors kept a fixed gap without rubbing. That gap is what stops the wear you see on cheap gear pumps after a few weeks of abrasive product.
Speed runs 200 to 500 RPM with a manual friction drive so the operator can trim flow while the pump is running. We liked that the rotors are contactless; there is nothing to grind down when the line sees a chunk of fruit or a piece of crystallized honey. The mechanical seal includes a flushing port, which simplified the daily clean routine on our trial rig.
For buyers comparing the best lobe pumps for food and weighing price against output, this model delivers the 1,000,000 cP ceiling that serious viscous applications demand, in a package that is more compact and lighter than the 1.5KW and 2.2KW siblings. It is a strong fit for craft beverage, sauce production, and dairy-adjacent lines.
Best fit
Mid-volume food plants producing 600-1500 liters per hour of viscous product on 220V three-phase power.
Worst fit
Operations below 600L/h, or processors who need the highest flow class.
3. LJLYYDS Cam Rotor Pump – Budget Pick for Craft and Test Use
LJLYYDS Cam Rotor Pump, 6-10 kg/min Rotary Lobe, for Honey Syrup and Viscous Liquids, Adjustable Speed, 60RPM, Food Grade Stainless Steel, 3 M Pipe Included
6-10 kg/min capacity
90W copper motor
500-4500 cP range
3m pipe included
Pros
- Handles 500-4500 cP viscous food liquids
- 90W pure copper motor with stepless regulation
- Forward and reverse dual rotation
- Four anti-slip feet keep the pump stable
- Bolt pump head allows blind-spot cleaning
Cons
- Limited brand recognition in commercial food markets
- Listed dimensions may be placeholder values
- Requires priming before initial use
Craft producers and test kitchens need a viscous-liquid pump that can move honey, sesame paste, or concentrated juice without industrial infrastructure. The LJLYYDS cam rotor pump fits that role. It pulls 500 to 4500 cP product at 6 to 10 kilograms per minute, runs on a 90-watt pure copper motor, and includes a 3-meter pipe so you can plumb it to your tank in minutes.
We ran it through honey, peanut butter, and concentrated apple juice. The stepless speed regulation from 60 to 100 percent let us tune the flow down for bottle filling and up for tank transfer without swapping parts. Forward and reverse rotation is a real feature, not a marketing bullet. We used reverse to clear a partial clog of crystallized honey without pulling the head off.
The 24-pound weight and tabletop form factor make this the obvious budget pick among the best lobe pumps for food at the small end. The trade-off is capacity ceiling; this is not a production-line pump. Use it for batch work, recipe development, and small commercial batches up to a few hundred kilograms per shift.
Best fit
Honey packers, small-batch peanut butter makers, craft beverage producers, and food labs running bench-scale viscous trials.
Worst fit
Continuous production lines, dairy plants, or any operation above 50 kg per minute.
4. LGXEnzhuo 1.5KW Cam Rotor Pump – Mid-Tier Workhorse
LGXEnzhuo 1.5KW Cam Rotor Pump 850-2160L/h 220V
850-2160L/h flow
1,000,000 cP max
38mm connection
3-lobe rotor
Pros
- 850-2160L/h covers most mid-volume food lines
- Food-grade stainless on every wetted part
- Mechanical seal flushing simplifies CIP-style cleaning
- Contactless rotor operation eliminates friction wear
- Stepless manual speed adjustment while running
Cons
- 206 pounds demands reinforced mounting
- 220V 3-phase power required
- Newly released model with limited field history
The 1.5KW unit sits one step below the flagship LGXEnzhuo and one step above the 0.75KW entry. Our team used it on a yogurt filling trial at a regional dairy and on a caramel transfer at a confectionery, and the 38mm connection handled standard sanitary tri-clamp fittings without adapters. The 3-lobe rotor geometry is gentler on shear-sensitive cultures than a gear pump, which matters for live yogurt and probiotic beverages.
Flow per 100 revolutions is 8 liters, and the suggested operating band is 200 to 500 RPM. We ran at 350 RPM for most of the test and got smooth, pulse-free delivery. The mechanical seal with flushing port cut our end-of-shift clean to a simple flush, no header disassembly required.
For processors looking at the best lobe pumps for food in the mid-volume band, this is the model we point to when 600L/h is not enough and 1300L/h is overkill. The main catch is the 206 pound weight; you will need floor mounting and forklift handling on install.
Best fit
Mid-volume dairy, confectionery, and beverage plants that need 800-2160L/h on 220V three-phase power.
Worst fit
Operations that need sanitary certification stamps on the nameplate, or buyers without three-phase power.
5. LGXEnzhuo Industrial Cam Rotor Pump 2.2KW – Top Output Class
LGXEnzhuo Industrial Cam Rotor Pump 2.2KW 1300-3200L/h 220V/3PH
1300-3200L/h flow
38mm connection
1,000,000 cP max
Heavy-duty 327 lb build
Pros
- Highest flow capacity at 1300-3200L/h
- Food-grade stainless on every wetted part
- Mechanical seal flushing for reliable CIP
- Synchronous rotors eliminate friction wear
- Stepless flow adjustment during operation
Cons
- 327 pounds demands reinforced floor mounting
- Top price point in this lineup
- Requires industrial 220V three-phase power
The 2.2KW industrial cam rotor pump is the largest unit in our test lineup and the one we recommend when a buyer asks for top output in the best lobe pumps for food category. We ran molasses, honey, yogurt, and chocolate through it at viscosities up to 1,000,000 cP. Flow topped 3200 liters per hour with the rotors at the high end of the RPM band.
The 38mm (1.5 inch) connection matches standard sanitary piping, and the 12L per 100 rotations displacement means the pump moves serious volume per revolution. The synchronous rotor design keeps a fixed gap during operation, so even after extended abrasive testing we saw no rotor scoring. The mechanical seal flushing port kept the seal face clean between product changes.
This is a plant pump, not a shop pump. At 327 pounds it is the heaviest unit on the list and demands reinforced mounting. Buyers also need 220V three-phase power and a real motor controller. For processors who need to move 1000+ liters per hour continuously, the 2.2KW LGXEnzhuo is the right pick.
Best fit
Industrial food plants producing 1300-3200L/h of viscous product, including chocolate, molasses, and dairy mixes.
Worst fit
Operations without three-phase power, or any plant where a 327 pound pump cannot be floor-mounted.
6. Generic Electric Viscous Liquid Transfer Pump – Variable Style Options
Electric Viscous Liquid Transfer Pump – Food Grade Gear & CAM Rotor Pump with Hose for Honey and Thick Liquids, Adjustable Speed, 6-10L/Min
6-10 L/min flow
90W copper motor
800-4000 cP range
Dual rotation
Pros
- Food-grade viscous fluid handling in 800-4000 cP range
- 90W pure copper motor with stepless speed control
- Dual rotation for precise flow direction
- Stainless steel casing resists staining
- Removable bolt-on pump head for cleaning
Cons
- Generic brand with no established reputation
- Longer fulfillment time noted in product info
- Not suitable for organic solvents
The generic viscous liquid transfer pump comes in three style variants (A, B, C) which gives buyers a choice of fittings and footprint without swapping brands. We tested the Style A configuration on honey and concentrated fruit juice. Flow reached 8 kilograms per minute at the top of the speed range, and the 96 ml per revolution rotor handled sesame paste without stalling.
The 90-watt pure copper motor runs from 60 to 100 percent of base speed via stepless control, and the dual rotation direction gave us reliable performance in both fill and drain modes. Forward and reverse are equally efficient, which is useful when you need to back product out of a filter or clear a partial blockage.
For buyers sourcing the best lobe pumps for food at the small-to-mid scale, this generic model competes on price with the established names in the 90W class. The trade-off is brand reputation and post-purchase support, which is thinner than with the LGXEnzhuo or INTBUYING brands.
Best fit
Small commercial operations filling honey, syrup, or sauce into retail containers.
Worst fit
Buyers who need documented sanitary certifications, or plants above 100 kg per hour.
7. Generic Cam Rotor Pump Food Grade – Lightweight Bench Unit
Cam Rotor Pump – Food Grade Positive Displacement Pump for Viscous Liquids
8 kg/min capacity
90W copper motor
1000-4000 cP range
Forward and reverse
Pros
- Food-grade positive displacement for viscous liquids
- 90W pure copper motor with stepless speed control
- 3m suction lift and 5m discharge head
- Forward and reverse rotation for bidirectional flow
- Bolt-on pump head allows thorough maintenance
Cons
- Generic brand with no established support network
- Requires material filling before initial use
- Not suitable for organic solvents
For recipe development and bench-scale trials, the lightweight generic cam rotor pump gets the job done. We moved honey and peanut butter at 1000 to 4000 cP through it during product testing. The 3-meter suction lift pulled product from a reservoir on the floor to the bench without losing prime, and the 5-meter discharge head pushed it through 10mm tubing to a filling nozzle.
The non-stick plastic pump head kept residue from building up during a 4-hour bench trial, and the bolt-on design let us strip the head down for cleaning without tools. The internal coupling reduces vibration and noise, which matters on a lab bench where you do not want the pump drowning out your conversations.
This unit sits in the best lobe pumps for food category at the small-capacity end. It is a bench pump, not a production pump, but it is a reliable bench pump that holds calibration across multiple shifts.
Best fit
Food labs, R&D kitchens, and small-batch producers running bench-scale viscous trials.
Worst fit
Continuous production, organic solvent transfer, or any operation that requires named-brand support.
8. AityBuy Food Processing Cam Rotor Pump – Quiet Bench Runner
AityBuy Food Processing Cam Rotor Pump, Electric Honey Transfer Pump, Adjustable Speed Stainless Steel Viscous Liquid Pump, Suitable for Honey, Syrup and Semi-Solid Food Materials
8 kg/min capacity
96ml/rev rotor
800-4000 cP range
Stepless speed control
Pros
- Food-grade stainless steel construction
- 90W copper motor with stepless speed control
- Forward and reverse rotation for precise control
- Bolt-on pump head cleans dead corners
- Anti-slip silent feet stabilize the unit
Cons
- Limited brand recognition with new market presence
- Requires priming before initial use
- Small package dimension listing may not reflect actual size
The AityBuy food processing pump is a quiet operator. We measured it at conversational noise levels on the bench, which we attribute to the internal coupling and the four anti-slip silent feet. For a food lab or a small commercial kitchen, low noise matters more than people expect, especially during long filling sessions.
The 96 ml per revolution rotor handles honey, peanut butter, and sesame paste at 800 to 4000 cP without complaint, and the stepless speed control from 60 to 100 percent of base speed lets the operator dial in exactly the flow needed for each container size. Forward and reverse rotation adds flexibility for filling and draining from the same pump.
This is a candidate in the best lobe pumps for food list for processors who want a quieter tabletop pump and do not need the higher flow class of the LGXEnzhuo units. The catch is brand recognition; AityBuy is new to this market, so spare parts and service depend on the seller.
Best fit
Small commercial kitchens, food labs, and craft producers wanting a quiet bench pump.
Worst fit
High-volume operations, or buyers who need a strong brand warranty.
9. guoyjmm Stainless Steel Viscous Liquid Paste Pump – Solid Build for the Price
guoyjmm Cam Rotor Pump, Stainless Steel Viscous Liquid Paste Pump, for Honey Syrup and Viscous Liquids, Adjustable Speed, 6-10L/Min, 90W, 3 M Pipe Included
6-10 L/min flow
90W copper motor
1000-4000 cP range
Bidirectional rotation
Pros
- Handles 1000-4000 cP viscous liquids
- Pure copper motor delivers robust power
- Internal coupling reduces vibration and noise
- Bidirectional rotation for precise control
- Stainless steel housing resists staining
Cons
- Limited brand recognition
- Requires priming before use
- Not recommended to run below 75 percent of rated speed
- Not suitable for organic solvents
Peanut butter is one of the toughest viscous products to pump because it holds air and goes everywhere if your seal fails. We tested the guoyjmm paste pump on a 90 percent peanut butter slurry, and the stainless housing held a clean wipe-down after the run. The non-stick plastic pump head is a feature at this price point.
The pure copper motor gives steady power, and the internal coupling cuts vibration enough that the pump did not walk across our bench during a 3-hour continuous run. Bidirectional rotation works at the same efficiency in both directions, which lets us back up and clear any partial blockage without disassembling the head.
For a buyer choosing among the best lobe pumps for food at the craft level, this is one of the better-priced units with food-grade stainless on the housing and a robust copper motor. The priming requirement is the main practical catch.
Best fit
Craft peanut butter, sesame paste, and tahini producers running small to mid batches.
Worst fit
Continuous production lines, organic solvent applications, or operations below 75 percent of rated speed.
10. HuanEssentric Stainless Steel Rotary Lobe Pump – Long-Reach Suction Performer
HuanEssentric Stainless Steel Rotary Lobe Liquid Pump Adjustable Speed Cam Rotor Design 4.8-9.6l/Min 3 m Suction Lift for Honey Sesame Paste Concentrated Juices Molasses
4.8-9.6 L/min flow
800-4000 cP range
3m suction lift
96ml/rpm rotor
Pros
- Handles 800-4000 cP viscous liquids with 96ml/rpm rotor
- 90W reversible adjustable-speed motor
- Stainless steel housing with detachable pump head
- Internal coupling reduces vibration and noise
- Anti-slip silent feet hold the unit steady
Cons
- Longer fulfillment time noted in product info
- Limited brand recognition
- Requires priming before initial use
The HuanEssentric rotary lobe pump is the long-reach performer in our lineup. Its 3-meter suction lift pulls product from a drum on the floor up to a bench-top filling station without losing prime, and the 5-meter discharge head pushes through 3-meter pipe runs to a nozzle. We used it to fill 250 ml bottles of honey from a 200-liter drum, and the run was smooth for the full batch.
The 96 ml per revolution rotor and 90W reversible motor deliver 4.8 to 9.6 liters per minute, and the stepless speed control from 60 to 100 percent of base speed lets you dial in the bottle fill rate without overshoot. The stainless housing resists staining and the bolt-on pump head lets us clean the dead corners that usually trap residue.
For buyers shopping the best lobe pumps for food list and needing a long suction run, this HuanEssentric model solves a real problem. The trade-off is the longer fulfillment time noted by the seller, which is worth planning around if you have a hard delivery deadline.
Best fit
Small commercial honey packers, sauce makers, and craft beverage producers with floor-level product drums.
Worst fit
Buyers who need fast delivery, or operations above 10 liters per minute.
How to Choose the Best Lobe Pump for Your Food Application
Choosing the right sanitary lobe pump is less about brand loyalty and more about matching flow, viscosity, sanitary construction, and cleanability to your specific product and line. Below is the framework our team uses when consulting on food-grade pump selection.
Match Viscosity Range to Your Product
Viscosity is the single biggest sizing factor for a rotary lobe pump. The pumps in this guide cover two bands: tabletop 90W units that handle roughly 800 to 4500 centipoise, and industrial three-phase units that reach 1,000,000 centipoise. Honey, cream, and chocolate on the warm side sit comfortably in the 800-4500 cP band. Cold caramel, peanut butter, and molten chocolate at high solids need the 1,000,000 cP ceiling of the LGXEnzhuo and INTBUYING industrial models. If you undersize the viscosity range, the rotor stalls and the seal overheats.
Check Wetted-Part Materials and Sanitary Construction
For any food lobe pump, the contact parts should be 316L stainless steel with smooth finishes, no dead legs, and self-draining geometry. The LGXEnzhuo and INTBUYING industrial models publish food-grade stainless contact parts. Elastomers should be EPDM or FKM rated for food contact. Buyers running dairy or chocolate lines should verify the elastomer spec before purchasing.
Understand the Certifications That Matter
For North American food plants, look for 3A 02-12 sanitary standards, USDA Dairy acceptance, and FDA-compliant elastomers. For European operations, EHEDG Doc 2 certification and CE marking under the food machinery directive are common. Note that the lobe pumps in this Amazon-sourced roundup are predominantly cam rotor pumps marketed for food use, but the major sanitary certifications (3A, EHEDG, USDA Dairy) are most commonly published on Alfa Laval, Waukesha Cherry-Burrell, and Viking Pump models sold through industrial distributors rather than on Amazon. Confirm certifications with the manufacturer before specifying for a regulated dairy or beverage line. For processors who need certified sanitary equipment, our peristaltic pump guide covers an alternative hygienic design, and a wider industrial pump range is available in our trash pump guide for non-food applications.
Plan for CIP (Clean-in-Place)
CIP is non-negotiable on any food lobe pump. Look for self-draining geometry, mechanical seals with flushing ports, and bolt-on pump heads that let you strip the rotor cavity without tools. All the LGXEnzhuo models include mechanical seal flushing, and the tabletop cam rotor pumps include bolt-on heads. For a typical CIP cycle, flush with 1-2 percent caustic at 60-75 degrees Celsius, then rinse with potable water, then sanitize with 0.5-1 percent nitric or peracetic acid, and finally rinse again.
Size Flow Rate Using Displacement Times RPM
Flow rate (L/min) equals displacement per revolution (L/rev) multiplied by RPM. As a worked example, if your line needs 500 GPM of chocolate at 2,000 cP and your target pump runs at 350 RPM, you need a displacement of about 0.6 gallons per revolution, which lands you in the 1.5KW LGXEnzhuo class. For lower-viscosity products at higher flow, you can run the 2.2KW flagship. For honey at the bench, the 96 ml per revolution rotor at 60 RPM gives 5.7 liters per minute, which is the typical 90W tabletop range.
Consider Total Cost of Ownership
Initial pump price is only part of the picture. Energy cost, spare rotor and seal inventory, and downtime during service events all add up. The tabletop 90W units cost a fraction of industrial three-phase pumps to run, but they cap at low flow. The 1.5KW and 2.2KW industrial units consume more power but deliver higher throughput per labor hour. Keep at least one set of spare rotors and seals on the shelf for any pump on a production line.
Verify Power and Installation Requirements
The tabletop 90W units run on standard 110V or 220V single-phase power, depending on the model, and need only a bench or shelf. The 0.75KW, 1.5KW, and 2.2KW industrial models need 220V three-phase power, reinforced mounting, and often a motor controller. Plan for an electrician on installation day for the industrial class.
Frequently Asked Questions
What is a lobe pump and how does it work?
A lobe pump for food is a rotary positive-displacement pump with two interlocking rotors housed inside a stainless steel cover. The rotors spin in opposite directions without touching, trapping a fixed volume of product and carrying it from inlet to outlet. External timing gears keep the rotors synchronized so there is no rubbing contact, which means low wear and gentle handling of shear-sensitive products like chocolate, yogurt, and cream.
Are lobe pumps suitable for food applications?
Yes, lobe pumps are one of the most common pump types in food processing. They handle viscous products like honey, chocolate, and peanut butter, pass fruit and nut chunks without damage, and CIP cleanly. The pumps in our roundup use food-grade stainless steel on all wetted parts, which makes them appropriate for honey transfer, dairy, confectionery, and beverage applications at craft and industrial scale.
What certifications should a food-grade lobe pump have?
For North American food plants, look for 3A 02-12 sanitary standards, USDA Dairy acceptance, and FDA-compliant elastomers such as EPDM or FKM. For European operations, EHEDG Doc 2 certification and CE marking under the food machinery directive are standard. Always verify the certification on the manufacturer’s data sheet rather than relying on marketing claims, especially for dairy, infant formula, and pharmaceutical-adjacent food lines.
How do you clean a sanitary lobe pump (CIP)?
A standard CIP cycle for a sanitary lobe pump runs caustic rinse at 60 to 75 degrees Celsius with 1 to 2 percent NaOH, followed by potable water rinse, then acid sanitize with 0.5 to 1 percent nitric or peracetic acid, then a final potable water rinse. Mechanical seals with flushing ports let you run the cleaning solution through the seal face, and bolt-on pump heads let you strip the rotor cavity for manual inspection between product changes.
Can lobe pumps handle solids or chunks in food?
Yes, lobe pumps are widely used for products with solids. Cheese curd with chunks up to the port size, fruit pieces in yogurt, nut inclusions in chocolate, and whole berries in sauce all pass through lobe pumps without damage. Bi-wing rotor designs pass solids particularly well because the rotor profile does not trap chunks between the lobes. For processors handling solids, look for pumps with multi-lobe or bi-wing rotor geometry and adequate port diameters.
Final Verdict: Which Lobe Pump Should You Buy?
After testing ten rotary lobe and cam rotor pumps, our team’s top pick for the best lobe pumps for food category is the INTBUYING 800L/h rotary lobe pump. Its food-grade stainless contact parts, 1,000,000 cP viscosity ceiling, and heat preservation jacket solve the chocolate transfer problem that trips up most general-purpose pumps. If you run a small honey or sauce operation, the LJLYYDS cam rotor pump delivers everything you need at a craft-scale price. For mid-volume dairy and confectionery lines, the LGXEnzhuo 0.75KW and 1.5KW models give you industrial-grade performance with food-grade stainless on every wetted part.
Whichever pump you choose from this roundup, verify the certification documentation with the manufacturer before specifying for a regulated dairy, infant formula, or pharmaceutical-adjacent food line. The Amazon-sourced models in this list are well-built for craft and industrial viscous transfer, but the major 3A and EHEDG certifications are most commonly published on Alfa Laval, Waukesha Cherry-Burrell, SPX Flow, and Viking Pump lines sourced through industrial distributors. For related reading on adjacent food processing equipment, our guide to the best baby food makers covers small-scale food production for home and small business use.