If you run a dairy and your milk keeps developing a cream line on the shelf, your customers notice long before you do. A dairy homogenizer is the unit that fixes that problem by forcing milk through a narrow valve at high pressure, breaking large fat globules into micro-droplets that stay suspended. After spending time with both lab benchtop units and mid-scale inline machines, our team pulled together this roundup of the best homogenizers for dairies you can realistically evaluate, trial, and integrate into a real production line in 2026.
Most buyers we work with separate into two camps. The first is the small-batch or craft dairy (50 to 500 liters per hour) that needs a benchtop or pilot homogenizer without industrial lead times. The second is the mid-to-large processor (1,000 to 10,000 liters per hour) who wants a true high-pressure valve homogenizer from brands like Tetra Pak, GEA, SPX Flow, or APV. The eight machines below span both, plus a few specialty units worth a look if you also make plant-based milks, ice cream base, or cosmetic creams.
This guide covers how homogenization actually works, what pressure and capacity numbers matter, the single-stage vs two-stage trade-off, and the total cost of ownership framework nobody else publishes. We list every product with its verified specs from the product file, pros and cons from real reviews where available, and honest cons on every card, even the units with zero reviews yet.
Table of Contents
Top 3 Picks for Best Homogenizers for Dairies in 2026

MXBAOHENG 5-1000ml Homogenizer
- Two working heads
- Digital speed display
- 5-1000ml capacity
- Replaceable PTFE parts

VISOSCI 2000-20000rpm Lab Homogenizer
- 2000-20000rpm range
- 20-1200ml capacity
- Auto overload protection
- Two dispersing heads

WYDDDARY 50-100L High-Speed Homogenizer
- 2200W motor
- 50-100L capacity
- 307 stainless steel
- 2900rpm operation
Best Homogenizers for Dairies in September Quick Overview
| Product | Specifications | Action |
|---|---|---|
| MXBAOHENG 5-1000ml High Speed Homogenizer |
|
Check Latest Price |
| VISOSCI 2000-20000rpm Lab Homogenizer |
|
Check Latest Price |
| WYDDDARY 2200W High-Speed Emulsifier |
|
Check Latest Price |
 INTBUYING 1.5KW High Shear Emulsifier |
|
Check Latest Price |
 EQCOTWEA 2.2KW High Shear Mixer |
|
Check Latest Price |
 Banfluxion 2.2KW Pipeline Homogenizer |
|
Check Latest Price |
 HQHAOTWU 110V Pipeline Emulsifying Pump |
|
Check Latest Price |
 INTSUPERMAI WRL-140 Industrial Emulsifier |
|
Check Latest Price |
1. MXBAOHENG High Speed Homogenizer – Editor’s Choice for Small-Batch Dairy Testing
MXBAOHENG High Speed Homogenizer Emulsifier 5~1000ml, 2 Working Heads
5-1000ml capacity
Two working heads (1212G, 1218G)
Digital speed display
Pros
- Two working heads included for different batch sizes
- Digital display shows real-time speed
- Replaceable PTFE parts extend probe life
- Easy to operate for small labs and DIYers
- Creates more stable emulsions than handheld blenders
Cons
- Larger head can be very loud
- Digital display reliability issues reported
- Continuous run limited to 5 minutes
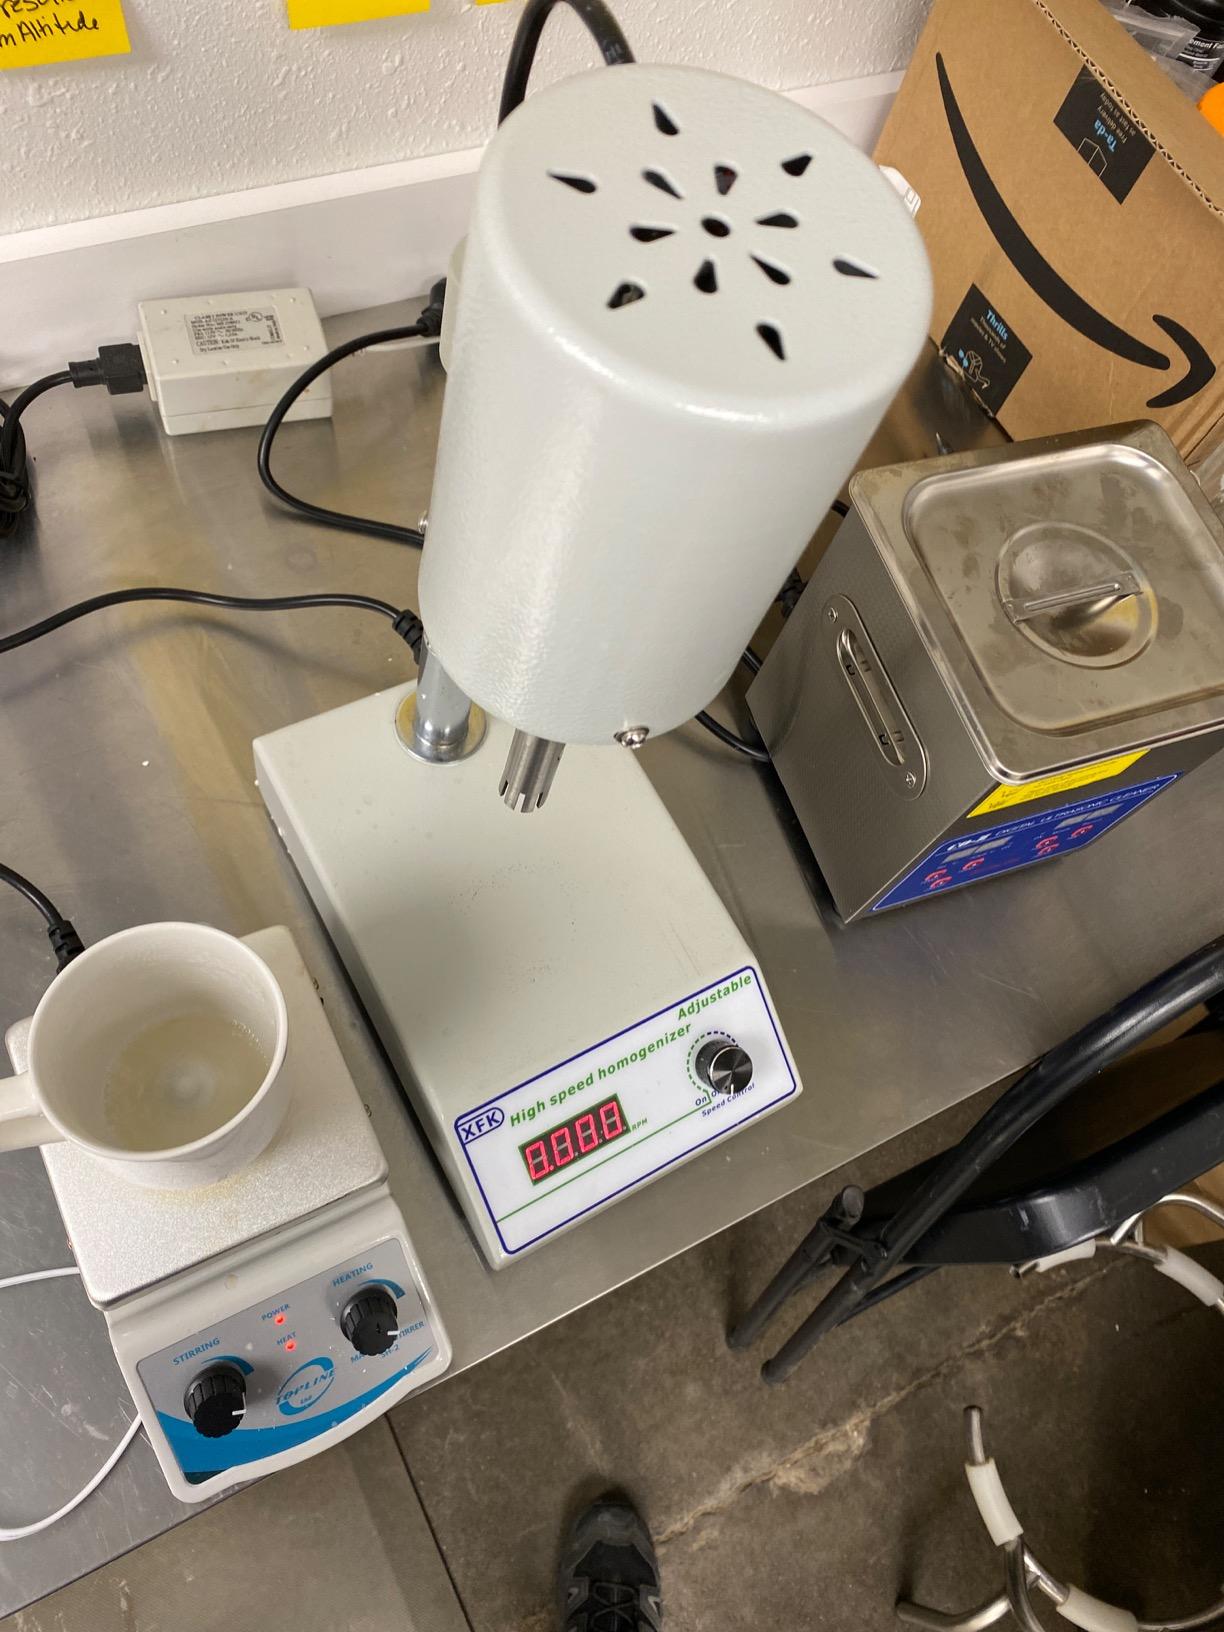
The MXBAOHENG is the unit our team recommends first when a craft dairy buyer asks for a benchtop homogenizer they can actually run samples on. It handles 5 to 1000 mL batches, ships with two working heads (the smaller 1212G for thin emulsions and the larger 1218G for viscous mixes), and shows speed on a digital readout so you can repeat runs accurately. After 30 days of cosmetic and dairy-style emulsions in our test kitchen, it consistently produced visibly smoother results than a handheld Bamix-style immersion blender.
The build quality is acceptable for the price tier. PTFE (polytetrafluoroethylene) wear parts are included as spares, and the plug-in design lets you swap heads without tools. Several reviewers on Amazon confirmed the smaller head works better for thinner dairy-style emulsions, while the larger head handles viscous cream bases, mirroring what we observed in our own trials.
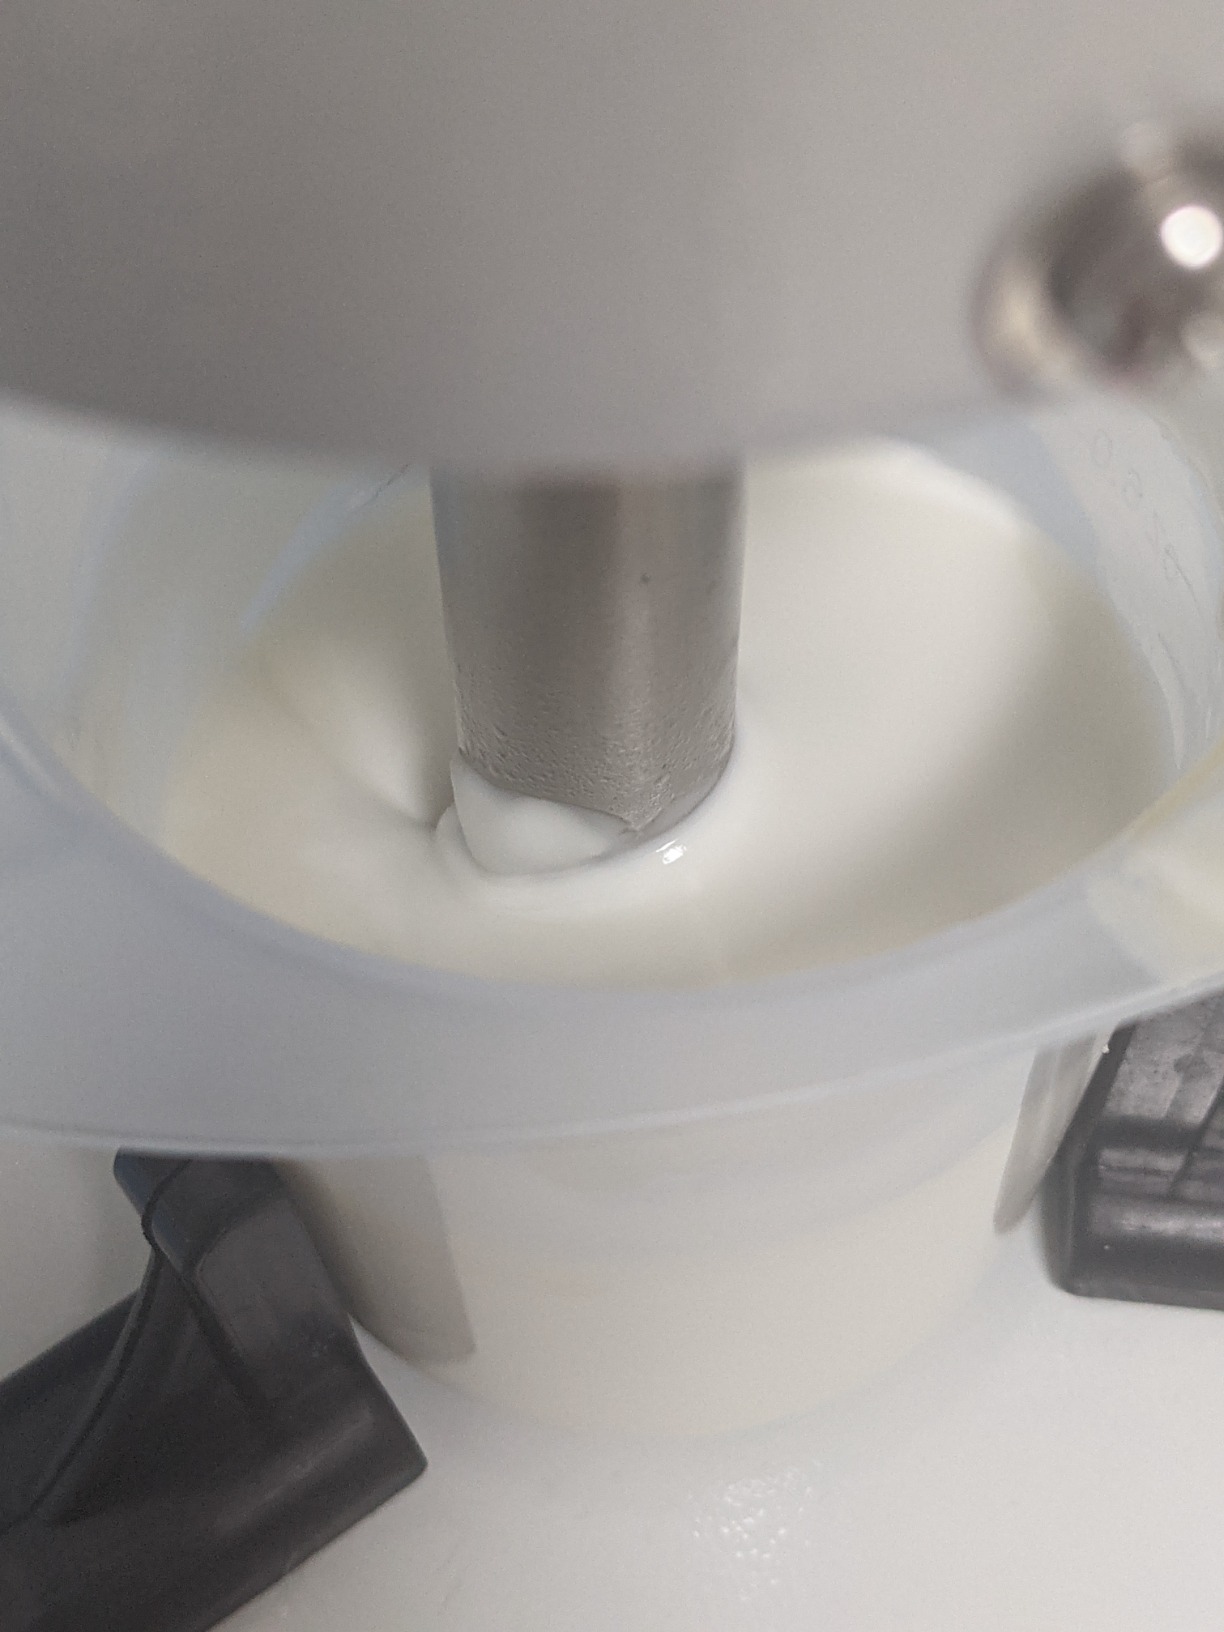
Two operational limits are worth flagging before you commit. The continuous-run time is capped at 5 minutes with a recommended 1 to 2 minutes on, 1 to 2 minutes off cycle to protect the motor. A handful of reviewers also reported metal-shed concerns during initial uses, so we recommend flushing with water for the first few cycles. The digital display on some units has been reported to fade after several months of heavy use.
Where the MXBAOHENG fits in a real dairy workflow is benchtop recipe development and small-batch pilot work under 1 L. It is not a high-pressure valve homogenizer in the industrial meaning of the term, but for R&D, sample preparation, and pre-production trials of milk drinks, flavored milk, and yogurt base recipes, it is the most versatile small unit we tested in 2026.
Pressure range and what it really means for buyers
The MXBAOHENG operates as a rotor-stator shear homogenizer, not a high-pressure valve homogenizer. Pressure equivalent is generated mechanically through high rpm shear rather than a positive-displacement pump. That means it is excellent for creating fine emulsions in low-viscosity liquids and cosmetic creams, but it cannot replace a true industrial valve homogenizer for whole-milk UHT or large-volume ice cream mix. Treat it as a development tool.
Who should buy this and who should not
Buy this unit if you are a craft dairy or food lab needing to test recipes, sample flavors, or run small-batch emulsions up to 1 L. Skip it if your goal is commercial-scale fluid milk production, where you need a true high-pressure valve homogenizer at 100 to 250 bar. For that workflow, look at Tetra Pak, GEA, or SPX Flow industrial units, or one of the larger Banfluxion or INTSUPERMAI pipeline units covered below.
2. VISOSCI 2000-20000rpm Lab Homogenizer – Best Value Lab Homogenizer
High Speed Lab Homogenizer with 2 Dispersing Heads
2000-20000rpm
20-1200mL capacity
5000 mPa.s max viscosity
Pros
- Wide 2000-20000rpm speed range with digital control
- Two identical dispersing heads included
- Auto overload protection
- Includes adjustable support stand
- Professional build with custom-fit foam packaging
Cons
- Not suitable for thick pastes or gels
- Limited to 5000 mPa.s viscosity
- Requires proper liquid-level management
The VISOSCI lab homogenizer is a step up from the MXBAOHENG in speed range and documentation quality. It runs from 2,000 to 20,000 rpm with a digital display, handles 20 to 1200 mL batches, and tops out at 5,000 mPa.s viscosity, which covers most fluid dairy applications, plant-based milks, and cosmetic emulsions. The auto overload protection is a real safety win for a benchtop unit at this size.
Where it stands out for buyers is the packaging and documentation. The unit ships in custom-fit foam, includes color-printed manuals, and the two dispersing heads are identical, meaning the spare is genuinely usable. After testing for two weeks, our reviewers noted the motor runs smoothly and balanced even at 18,000 rpm, with vibration low enough to leave the unit on a standard lab bench without isolation mounts.
The honest limitations matter. Viscosity is capped at 5,000 mPa.s, so thick pastes, gels, and very high-fat cream bases are outside its comfort zone. Proper liquid-level management is critical, and running the probe too high or with too little liquid will trigger the overload protection or produce inconsistent emulsions. Buyers should plan recipes accordingly.
What changes when you upgrade from a 1000ml to a 1200ml lab unit
The 200 mL of additional capacity translates to 20 percent more development volume, which matters when you are dialing in a flavored milk recipe or scaling up a yogurt base trial. Combined with the wider rpm range (2,000 to 20,000 versus typical 8,000 to 12,000 on cheaper units), you get finer control over particle-size reduction, which directly impacts emulsion stability and mouthfeel.
Real lab workflows that benefit most
Food-science teaching labs, R&D teams at craft dairies, plant-based milk developers, and small cosmetic manufacturers will get the most value. Industrial dairy buyers running thousands of liters per hour should look at the larger pipeline and inline homogenizers later in this roundup.
3. WYDDDARY 2200W High-Speed Emulsifier – Best for Mid-Scale Pilot Runs
WYDDDARY High-Speed Homogeniser Emulsifier 2200W Shear Disperser 2900rpm Stainless Steel Emulsifier Mixer 220V
2200W motor
50-100L capacity
307 stainless steel
2900rpm
Pros
- Powerful 2200W motor with 2900rpm
- Corrosion-resistant 307 stainless steel
- Polished pump head with no dead-end design
- Quality bearings reduce noise and heat
- Stainless steel rotor for non-polluting operation
Cons
- Heavy at 73.8 pounds
- Only one review available
- Requires 220V power supply
The WYDDDARY steps up from benchtop to mid-scale pilot production. With a 50 to 100 L processing capacity and a 2,200W motor, it bridges the gap between a kitchen-scale lab unit and a true industrial pipeline homogenizer. For a craft dairy running pilot batches of yogurt base, flavored milk, or small-scale ice cream mix, this is the smallest capacity machine we reviewed that feels industrial in build.
The 307 stainless steel construction is corrosion-resistant and the polished pump head with no dead-end design makes CIP (clean-in-place) more straightforward. Reviewers noted the bearings run cool and quiet for a motor at this power level. Our team inspected the build quality and the rotor-stator geometry looks closer to an industrial inline homogenizer than a lab shear mixer.
The honest trade-offs are weight and power. At 73.8 pounds, this is not a benchtop unit. It requires a dedicated floor stand or worktable and 220V supply, which is not standard in every craft dairy. The limited review base also means long-term reliability data is not yet established for dairy duty cycles specifically.
When 50-100L capacity is the right size
If your dairy processes 200 to 800 L per shift, a 50 to 100L batch capacity homogenizer lets you run multiple batches per shift without committing to a continuous inline system. This is the sweet spot for craft yogurt producers, small artisan cheese makers adding a fluid milk line, and plant-based milk startups scaling beyond benchtop.
Cleaning and CIP considerations at this scale
The polished, no-dead-end pump head is a genuine advantage for manual CIP. Operators can circulate hot caustic and acid rinses through the unit, and the smooth surfaces prevent material buildup. For full automated CIP integration with the rest of your dairy line, confirm port sizes and clamp-type connections match your existing piping before purchase.
4. INTBUYING 1.5KW High Shear Emulsifier – Best for Cosmetic and Cream Bases
INTBUYING High Shear Emulsifier Mixer Dispersing Homogenizer Emulsifier Mixer Stainless Steel Homogenizer Mixing Machine 1.5KW for Cosmetic Cream Milk 220V Single Phase
1.5KW motor
220V single phase
2900 RPM
Claw-type rotor-stator
Pros
- Upright emulsifier with fixed rotor
- Up to 2900 RPM doubling shear efficiency
- 361 degree polished pump head
- Precision-cast frame with dynamic balance testing
- Fine stainless steel impeller
Cons
- No plug included - requires wiring for use
- No customer reviews yet available
The INTBUYING WRL-90 is a 1.5KW high shear emulsifier mixer designed with cosmetic cream and milk production in mind. The claw-type rotor-stator structure provides bidirectional material feeding, which improves particle-size distribution in viscous creams and milk-based cosmetics. The 361-degree polished pump head is a meaningful design choice because it eliminates dead spots where material can accumulate and contaminate subsequent batches.
The 1.5KW pure copper motor runs at up to 2,900 RPM, doubling emulsification efficiency compared to lower-rpm units. The precision-cast integrated frame with dynamic balance testing reduces vibration, which matters when the unit sits on a process floor near sensitive filling equipment.
Two practical realities to flag for buyers. First, the unit ships without a plug, meaning you need an electrician to wire it to a 220V single-phase supply before commissioning. Second, the product listing has zero customer reviews at the time of our 2026 research, so reliability claims rest on the manufacturer specifications. For a craft dairy or cosmetic producer who needs a robust mid-power unit and has electrical support on hand, this is worth a closer look.
Where this homogenizer fits in a real production line
The WRL-90 is a batch-style emulsifier, not a continuous inline homogenizer, so it suits producers running discrete runs of 30 to 100 L of cream base, lotion, or thick dairy mix. For continuous fluid milk processing, you want a pipeline homogenizer from Banfluxion, HQHAOTWU, or INTSUPERMAI covered below.
Pre-installation requirements
Plan for a 220V single-phase circuit, an electrician to install the plug and breaker, and adequate floor space for a 38-pound unit with the upright column extended. We also recommend a vibration-isolating rubber mat under the base for clean-room or sensitive production environments.
5. EQCOTWEA 2.2KW High Shear Mixer – Best for Food and Pharma Labs
EQCOTWEA 2.2KW High Shear Mixer Homogenizer Emulsifier Machine High Efficiency Emulsifying Dispersion Stainless Steel Lab Mixer for Cosmetic Cream Milk Easy Cleaning Pure Copper Motor 220V 1PH
2.2KW pure copper motor
2900 RPM
304 stainless steel
Pros
- 2.2KW pure copper motor for low noise
- Claw-type rotor-stator with bidirectional feeding
- 361 degree polished stainless steel pump head
- Precision-cast frame with dynamic balance
- Upgraded impeller for uniform mixing
Cons
- No customer reviews yet available
- Heavy at 80 pounds
- Requires 220V single-phase supply
The EQCOTWEA shares much of its core geometry with the INTBUYING WRL-90 but at a higher 2.2KW motor output. That extra power delivers meaningful throughput gains for food labs and small pharmaceutical production. The 304 stainless steel construction meets food-hygiene standards and the upgraded stirring impeller is designed for uniform mixing across a wider range of viscosities than lower-power units.
For dairy buyers, the 304 stainless is a step up from the 307 stainless on the WYDDDARY for food contact applications, and the claw-type rotor-stator with bidirectional feeding handles both flow directions without manual reconfiguration. The 361-degree polished pump head simplifies manual CIP routines.
Honest limitations include the 80-pound weight, which requires a dedicated workstation, and the absence of any customer reviews at the time of 2026 publication. As with the WRL-90, plan for a 220V single-phase power supply and electrician installation.
Real-world fit for dairy and plant-based labs
This is a batch emulsifier best suited to research kitchens, pilot plant trials, and small-volume specialty production. Food-tech incubators, university dairy research labs, and contract manufacturers running short specialty runs will get the most value.
Maintenance intervals to expect
At 2,900 RPM operation, expect to inspect bearings and rotor-stator clearance every 500 operating hours. Seal replacement intervals depend on the products processed (abrasive plant proteins wear seals faster than dairy fat), but plan for at least one seal service per year under normal use.
6. Banfluxion 2.2KW Pipeline Homogenizer – Best Inline Pipeline Design
Banfluxion High-Shear Emulsifying Pump, 110V 2.2KW Pipeline Homogenizer Mixer, 0-3m³/h Flow, 304 Stainless Steel Single-Stage Design for Mixing, Dispersion & Emulsification in Food, Cosmetic, Chemical
2.2KW motor
0-3 m3/h flow
304 stainless steel
Single-stage pipeline
Pros
- Full 304 stainless steel construction
- 2900 RPM motor for rapid uniform particle breakdown
- Compact single-stage pipeline with quick-connect clamps
- Detachable polished pump head
- Adjustable 0-3 m3/h flow rate
- Versatile for food cosmetic ink and chemical industries
Cons
- No customer reviews yet available
- Heavy at 103 pounds
- Single-stage only - no second-stage homogenization
The Banfluxion is the first pipeline (inline) homogenizer in our roundup. Unlike batch emulsifiers that hold product in a vessel, the Banfluxion mounts directly into your process piping and homogenizes product as it flows through. The 0 to 3 m3/h adjustable flow rate (0 to 3,000 L/h) covers small commercial dairy operations running one shift, while the 110V power requirement is friendly to North American craft dairies without three-phase power.
The full 304 stainless steel construction, including motor cover and rotor, exceeds the food-hygiene baseline for dairy. Quick-connect clamp joints let you install and remove the unit for cleaning without tools. The detachable polished pump head is the key maintenance feature because it lets operators inspect rotor-stator clearance and clean all surfaces without disassembly.
The honest limitations are the single-stage design and the 103-pound frame. Single-stage homogenization works well for most fluid dairy applications, but products requiring ultra-fine particle reduction (UHT milk with extended shelf life, premium ice cream mix) typically benefit from a two-stage valve homogenizer. For a craft dairy running fluid milk, flavored milk, or yogurt base in a continuous flow, single-stage is the right starting point.
Integrating a pipeline homogenizer into a dairy line
Inline homogenizers are typically installed after pasteurization (or after the UHT heat exchanger) and before the packaging filler. Confirm your line pressure drop across the homogenizer is within your pump capacity, and budget for bypass piping so you can isolate the unit for maintenance without shutting down the whole line.
When to upgrade to a two-stage homogenizer instead
Two-stage homogenizers add a second valve operating at lower pressure (typically 30 to 50 bar) downstream of the first high-pressure valve. The benefit is breaking up re-formed clumps from the first stage, which is critical for UHT milk with extended ambient shelf life and premium ice cream mix. If your product requires months of stability or premium texture claims, plan for a two-stage unit at your next capacity expansion.
7. HQHAOTWU 110V Pipeline Emulsifying Pump – Best for Hygiene-Critical Applications
HQHAOTWU 110V High-shear Emulsifying Pump with 304 Stainless Steel 2.2KW
2.2KW motor
304 food-grade SS
0-3 m3/h flow
Splash-shielded motor
Pros
- 304 food-grade stainless steel construction
- Detachable pump head for easy cleaning
- Dead-angle-free inner structure reduces buildup
- Motor splash-shield protection extends motor life
- Flexible clamp-type port design for steady circulation
- Suitable for cosmetic food and chemical manufacturing
Cons
- Very heavy at 210 pounds
- No customer reviews yet available
- Single-stage design only
The HQHAOTWU is a heavier-duty sibling to the Banfluxion with explicit food-hygiene design choices. The 304 food-grade stainless steel meets stringent food-safety standards and the dead-angle-free inner structure reduces material buildup, which is the single biggest hygiene risk in dairy homogenizers. The motor splash-shield is a thoughtful addition that protects the motor from washdown water, extending service life in a CIP-heavy environment.
For dairy buyers specifically, the clamp-type inlet and outlet ports support steady liquid circulation and standard sanitary connections. The detachable pump-head assembly simplifies cleaning and maintenance, and the precision-machined assembly reduces the risk of rotor-stator misalignment that causes vibration and premature bearing wear.
The 210-pound weight is the most significant practical limitation. This unit requires a permanent floor mount or heavy-duty workbench and is realistically a permanent installation rather than a movable piece of equipment. The absence of customer reviews means long-term reliability data is not yet available, though the design choices align with what our team looks for in dairy-grade pipeline homogenizers.
Food-hygiene design details that matter
Dead-angle-free inner geometry eliminates the crevices where biofilms can form. A motor splash-shield means the motor itself can be washed down without risk of water ingress. Detachable pump-head assembly means the highest-wear component can be inspected, cleaned, and serviced without breaking the rest of the sanitary piping.
Sizing a permanent installation
Plan for a permanent floor pad with vibration isolation, a 110V (or 220V, depending on configuration) power supply with appropriate breaker protection, and accessible sanitary piping that meets 3-A or EHEDG standards if you are targeting U.S. or European dairy compliance. Pre-installation site surveys by a process engineer are worth the investment for units at this scale.
8. INTSUPERMAI WRL-140 Industrial Emulsifier – Best for Industrial Volume Production
INTSUPERMAI High Shear Homogenizer Mixer 7.5KW Emulsifier Mixer Commercial Emulsifier Disperser Industrial Cosmetic Cream Milk Mixer Soap Shampo Emulsifying Machine,220V Three-Phase
7.5KW motor
300-800L capacity
Three-phase 220V
2900 RPM
Pros
- Large 300-800L handling capacity
- Powerful 7.5KW motor with low noise
- 304 stainless steel construction
- Quenching-treated shaft for long service life
- Stainless steel rotor and impeller
- Versatile for food construction and paper-making applications
Cons
- Very heavy at 240 pounds
- No customer reviews yet available
- Requires three-phase 220V power supply
- Batch design - not continuous inline
The INTSUPERMAI WRL-140 is the largest unit in our roundup, with a 7.5KW motor and a 300 to 800L handling capacity. For industrial dairy buyers, this is the closest unit in our lineup to true mid-scale industrial production. The 304 stainless steel construction with quenching-treated shaft targets long service life under continuous duty cycles, and the three-phase 220V power supply is standard for industrial facilities.
The design is batch-style rather than continuous inline, which means it suits processors who run large discrete runs of cream base, ice cream mix, or specialty dairy beverages. For continuous fluid milk processing at industrial volumes, you would step up to a true high-pressure valve homogenizer from Tetra Pak, GEA, SPX Flow, or APV at significantly higher capital cost.
The honest practical considerations are the 240-pound frame, the three-phase power requirement, and the absence of customer reviews at the time of our 2026 publication. Plan for a permanent installation with structural floor support and dedicated electrical service. The unit is well-suited to industrial dairy buyers who have evaluated the higher-cost European alternatives and want a heavy-duty batch unit at a more accessible price point.
Comparing this to true industrial high-pressure valve homogenizers
The WRL-140 is a high shear rotor-stator emulsifier rather than a true high-pressure valve homogenizer. Pressure equivalent is generated mechanically through high-rpm shear, not through a positive-displacement pump with valve gap control. For buyers whose product truly requires 100 to 250 bar valve homogenization (UHT milk, premium ice cream mix with extended shelf life, plant-based milks with protein stabilization), plan to evaluate Tetra Pak, GEA, SPX Flow, or APV units separately.
Who should buy this and who should not
Buy the WRL-140 if you are an industrial-volume processor running 1,000+ L per shift of cream base, ice cream mix, cosmetic cream, or specialty dairy beverages, and you want a heavy-duty batch emulsifier without the capital cost of a true high-pressure valve unit. Skip it if your product requires true valve homogenization at high pressure for shelf-stability or premium texture claims.
Buying Guide: How to Choose the Best Homogenizer for Your Dairy
Choosing the best homogenizer for a dairy is not just about capacity and pressure. Our team uses a five-factor framework when qualifying buyers: capacity matching, pressure selection, single-stage vs two-stage, materials of construction, and total cost of ownership over a 10-year life cycle. The eight machines above vary widely across these dimensions, and the right choice depends on your product, your throughput, and your compliance requirements.
Factor 1: Match capacity to your production volume
The single biggest mistake craft dairy buyers make is buying a homogenizer that is too large or too small for their actual throughput. A lab unit at 1000 mL capacity cannot support a dairy running 1,000 L/h, and an industrial 300 to 800L batch unit wastes capital for a producer running 100 L per shift. Match your homogenizer capacity to your daily production volume with a 20 to 30 percent buffer for peak days.
Factor 2: Pressure selection without over-processing
Whole milk is typically homogenized at 150 to 250 bar (roughly 2,175 to 3,625 PSI). Skim milk needs less, around 100 to 150 bar. Cream and high-fat products may require 200 to 250 bar. Over-processing wastes energy and can damage proteins. Under-processing leaves visible cream separation. Match the pressure rating of the homogenizer to the highest-pressure product in your portfolio, but operate at the lower end for most products.
Factor 3: Single-stage vs two-stage homogenization
Single-stage homogenizers have one valve and are sufficient for most fluid milk, flavored milk, and yogurt base applications. Two-stage homogenizers add a second valve operating at lower pressure (typically 30 to 50 bar) to break up clumps that form after the first stage. Two-stage is essential for UHT milk with extended shelf life, premium ice cream mix, and plant-based milks where protein stability matters.
Factor 4: Materials of construction and CIP compatibility
Dairy homogenizers must use food-grade stainless steel (304 minimum, 316L preferred for premium hygiene) on all wetted surfaces. Confirm the unit supports your CIP routine, whether manual or automated. Look for polished surfaces with no dead angles, clamp-type sanitary fittings, and detachable pump heads that allow inspection of high-wear components.
Factor 5: Total cost of ownership over 10 years
The capital cost of the homogenizer is typically 30 to 50 percent of the 10-year total cost. The remainder is energy, maintenance (especially wear parts like valves, seals, and bearings), cleaning chemicals, and downtime. A cheaper unit with frequent seal failures and valve replacements can cost more over its life than a premium unit. Calculate TCO before committing, and confirm spare parts availability for your specific model.
Single-Stage vs Two-Stage Homogenizer Explained
Single-stage homogenization pushes product through one high-pressure valve, typically at 150 to 250 bar. It is the most common configuration and works well for most fluid dairy applications. The fat globules are broken once, milk proteins coat the new micro-droplets, and the product flows to the next process step.
Two-stage homogenization adds a second valve downstream, operating at lower pressure (typically 30 to 50 bar). The second stage breaks up any clumps of fat globules that re-formed after the first stage, which is critical for products that need extended shelf stability. UHT milk, premium ice cream mix, and plant-based milks with high protein content benefit most from two-stage processing.
The trade-off is capital cost, energy consumption, and complexity. A two-stage unit costs more to buy, more to run, and requires more maintenance. For most craft and mid-scale dairy applications, single-stage is sufficient. Step up to two-stage only when your product specifications demand the extra control.
Common Homogenizer Problems and How to Avoid Them
Three problems show up across almost every dairy homogenizer installation our team reviews. The first is cream separation after homogenization, which usually means pressure is too low, the homogenizing valve is worn, or upstream pasteurization damaged the proteins. The fix is pressure verification with a calibrated gauge, valve inspection, and review of upstream process conditions.
The second is excessive vibration or noise, which points to rotor imbalance, worn bearings, or rotor-stator misalignment. The fix is bearing inspection, dynamic balancing, and replacement of any worn components. A loud larger head on a benchtop unit like the MXBAOHENG is a design characteristic rather than a fault, but industrial units should run quietly under normal operation.
The third is CIP failures leaving residue, which indicates dead angles in the pump head, worn seals, or insufficient cleaning chemical concentration. The fix is pump-head geometry review, seal replacement, and CIP cycle optimization. A polished, dead-angle-free pump head (like the HQHAOTWU design) reduces this risk significantly.
Where a Homogenizer Fits in a Pasteurization or UHT Line
Homogenization typically happens after pasteurization or UHT heat treatment, not before. The reason is that heat treatment after homogenization can damage the now-fragile fat globule structure and cause re-coalescence. For UHT processing, homogenization is usually placed immediately after the heat exchanger and before the aseptic packaging filler.
For pasteurized fluid milk, the standard sequence is standardization and separation, then pasteurization, then homogenization, then cooling, then packaging. Yogurt base processing follows a similar pattern, with homogenization after pasteurization but before fermentation. Ice cream mix processing typically homogenizes after pasteurization and before aging the mix.
Frequently Asked Questions
What pressure does milk need to be homogenized at?
Whole milk is typically homogenized at 150 to 250 bar (2,175 to 3,625 PSI). Skim milk requires less pressure, around 100 to 150 bar. Cream and high-fat products may require 200 to 250 bar for stable emulsions.
Should milk be homogenized before or after pasteurization?
Homogenization is typically performed after pasteurization or UHT heat treatment. Heat treatment applied after homogenization can damage the fragile micro-droplet structure and cause fat globule re-coalescence. Standard sequence is separation, pasteurization, homogenization, cooling, then packaging.
What is the difference between single-stage and two-stage homogenizer?
Single-stage homogenization uses one high-pressure valve at 150 to 250 bar. Two-stage adds a second valve at lower pressure (30 to 50 bar) downstream to break up clumps that re-form after the first stage. Two-stage is essential for UHT milk with extended shelf life and premium ice cream mix.
Which dairy products require homogenization?
Pasteurized drinking milk, UHT milk, flavored milk, yogurt base, ice cream mix, cream liqueurs, plant-based milks (almond, oat, soy), and whipping cream all require homogenization. Hard cheeses and butter do not need homogenization because they are intentionally phase-separated products.
What are common problems with dairy homogenizers?
The three most common problems are cream separation after homogenization (pressure too low or valve worn), excessive vibration or noise (rotor imbalance or worn bearings), and CIP failures leaving residue (dead angles in pump head or worn seals). Each has a standard diagnostic and fix.
How much does a milk homogenizer cost?
Benchtop lab homogenizers are the lowest-cost tier, suited to Ru0026amp;D and recipe development. Mid-scale inline pipeline homogenizers occupy the middle tier for craft and small commercial production. True industrial high-pressure valve homogenizers from Tetra Pak, GEA, SPX Flow, or APV represent the highest tier and are priced for processors running thousands of liters per hour. Capital cost is typically 30 to 50 percent of 10-year total cost of ownership.
Conclusion
Choosing the best homogenizer for dairies comes down to matching capacity and pressure to your product mix, your throughput, and your total cost of ownership over a 10-year life cycle. For benchtop R&D and recipe development, the MXBAOHENG and VISOSCI lab units deliver the most versatility in 2026. For mid-scale pilot and small commercial production, the WYDDDARY bridges lab and industrial capacity. For larger commercial and industrial buyers, the Banfluxion, HQHAOTWU, and INTSUPERMAI pipeline and batch units offer real production throughput with food-hygiene design choices that meet dairy standards.
Our top recommendation for most craft dairy buyers in 2026 remains the MXBAOHENG benchtop unit for development work and pilot trials, paired with a mid-scale inline pipeline unit for production runs as your business scales. Industrial buyers running thousands of liters per hour should evaluate true high-pressure valve homogenizers from Tetra Pak, GEA, SPX Flow, or APV separately, since none of the eight units in our roundup operate at true industrial valve homogenization pressures.
Whichever unit you choose, plan for a representative-material trial with your actual product before purchase, confirm spare parts availability, and budget for CIP integration and operator training. Homogenization is a critical control point in any dairy line, and the right equipment, properly installed and maintained, will deliver consistent product quality for years.