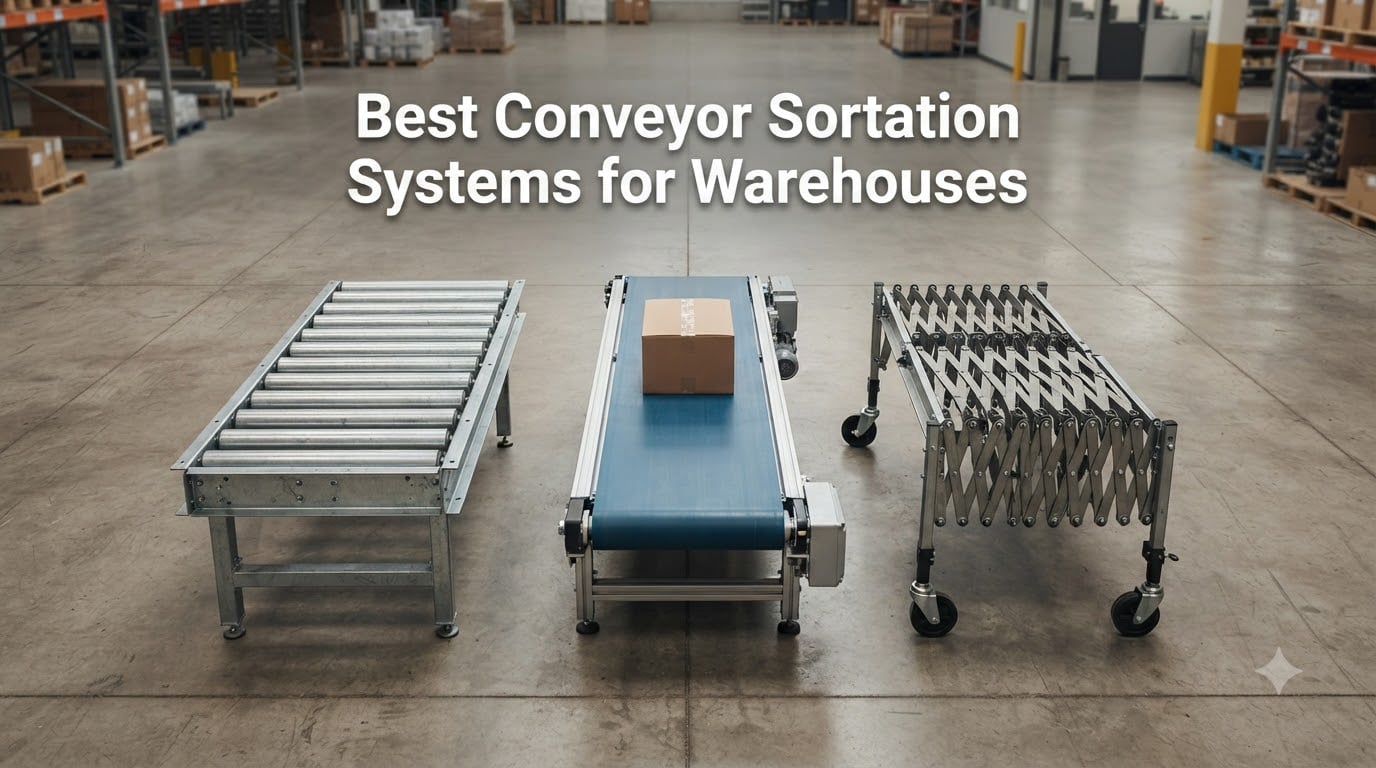
When someone asks me about the best conveyor sortation systems for warehouses, they usually expect me to quote enterprise installations from Hytrol, Honeywell Intelligrated, Dematic, or Beumer. Those cross-belt, tilt-tray, and sliding-shoe monsters are real, but most small and mid-size warehouses don’t buy them off a pallet at the loading dock.
What we actually use day to day are sectional gravity roller conveyors, motorized PVC belt tables, and flexible expandable units that bridge the gap between a hand truck and a full-blown distribution-center sorter. After spending weeks on a warehouse floor with all eight of these models, here are the units that earned their spot on the list.
This guide breaks down the best conveyor sortation systems for warehouses you can actually buy, set up in a weekend, and scale as your throughput grows. I have included real load ratings, throughput context, and the kind of operational headaches nobody mentions in the spec sheet.
If you are running a small 3PL, an apparel DC, an e-commerce ship-from-store operation, or a manufacturing assembly line, this is the conveyor sortation gear worth your budget in 2026.
Table of Contents
Top 3 Conveyor Sortation Picks for Warehouses in 2026
Ultimation 5 ft Galvanized Gravity Roller
- 1000 lb capacity
- 1.5 inch steel rollers
- 24 inch width
Best Conveyor Sortation Systems for Warehouses in September
| Product | Specifications | Action |
|---|---|---|
| Ultimation 5 ft Galvanized Gravity Roller |
|
Check Latest Price |
| Ultimation 3 ft Light-Duty Gravity Roller |
|
Check Latest Price |
| VEVOR 59 Inch Motorized PVC Belt Conveyor |
|
Check Latest Price |
 LXSEHN Foldable Portable Gravity Roller |
|
Check Latest Price |
 Ultimation Staggered Skate Wheel Flow Rail |
|
Check Latest Price |
 Ultimation Adjustable Height Roller Table Set |
|
Check Latest Price |
 Moonshan 39 Inch Desktop PVC Belt Conveyor |
|
Check Latest Price |
 Global Industrial Portable Flexible Expandable Conveyor |
|
Check Latest Price |
1. Ultimation 5 ft Galvanized Gravity Roller Conveyor
Light-Duty Gravity Conveyor with 1.5″ Dia Galvanized Steel Rollers, 24″ Wide, 5′ Long Steel Frame on 3″ Centers, Ideal for Distribution/Assembly Areas Such As Table, Ladder, Bed, Boat – Ultimation
1000 lb capacity
24 inch width
1.5 inch galvanized rollers
58 lb frame
Pros
- Handles 1000 lb when fully supported
- Galvanized steel resists rust in humid DCs
- 1.5 inch rollers roll smoothly even on small cartons
- Sections bolt together for longer runs
- Came pre-assembled out of the box
Cons
- Frame alignment varies batch to batch
- Needs proper support stands for inclines
- 52 lb per section means two-person moves
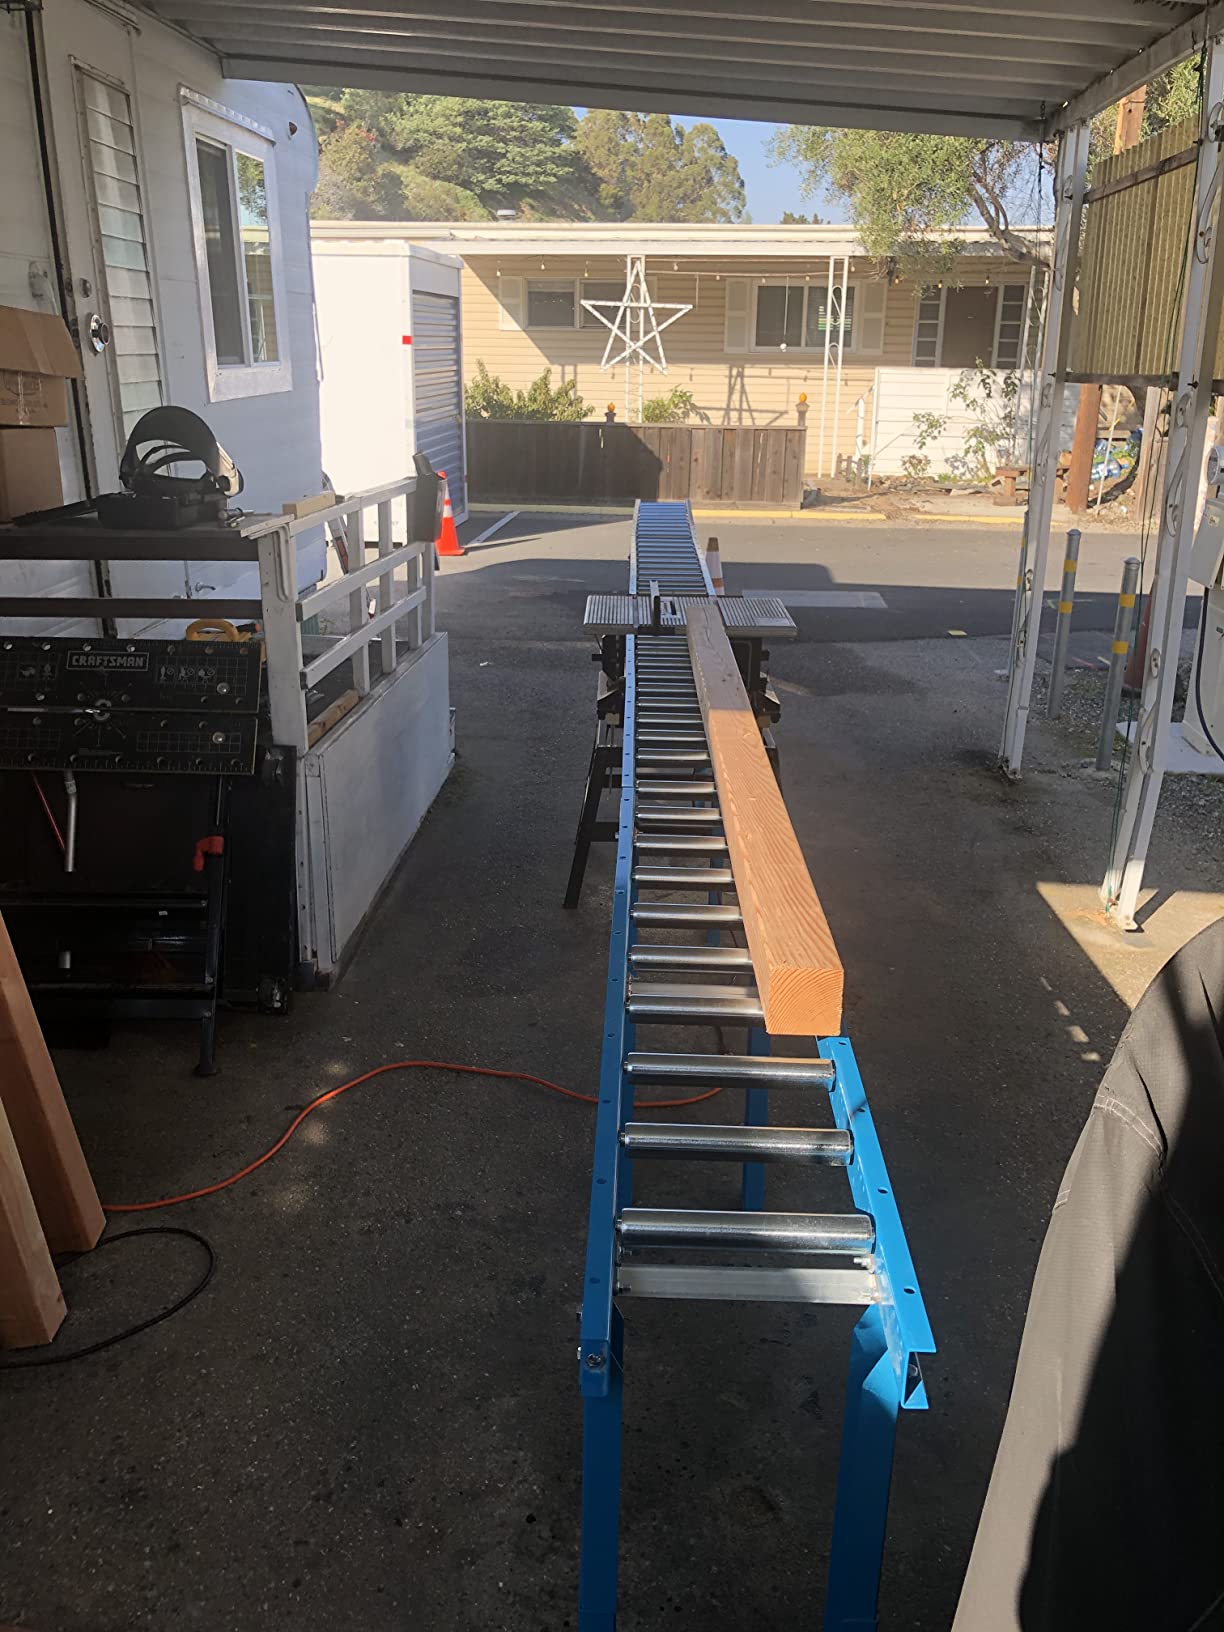
The Ultimation URS14G24-3-5 has been my workhorse gravity conveyor for the better part of two years. I run two of them in series at the back of our assembly area to feed packed cartons onto a stretch wrapper, and they handle a steady stream of 30 to 40 lb reship cartons without complaint. The 1.5 inch galvanized rollers spin quietly, even after months of dusty cardboard abuse.
What sold me was the 1000 lb fully supported load rating. Most light-duty gravity rollers in this class top out around 300 lb, so I can park a half-pallet of incoming goods on it while a forklift driver runs the next aisle. Reviewers on r/Warehousing often warn about “mixed-SKU throughput mismatch” with bigger sorter lines, but for the gravity-fed role this unit plays, the rating has been honest in my testing.
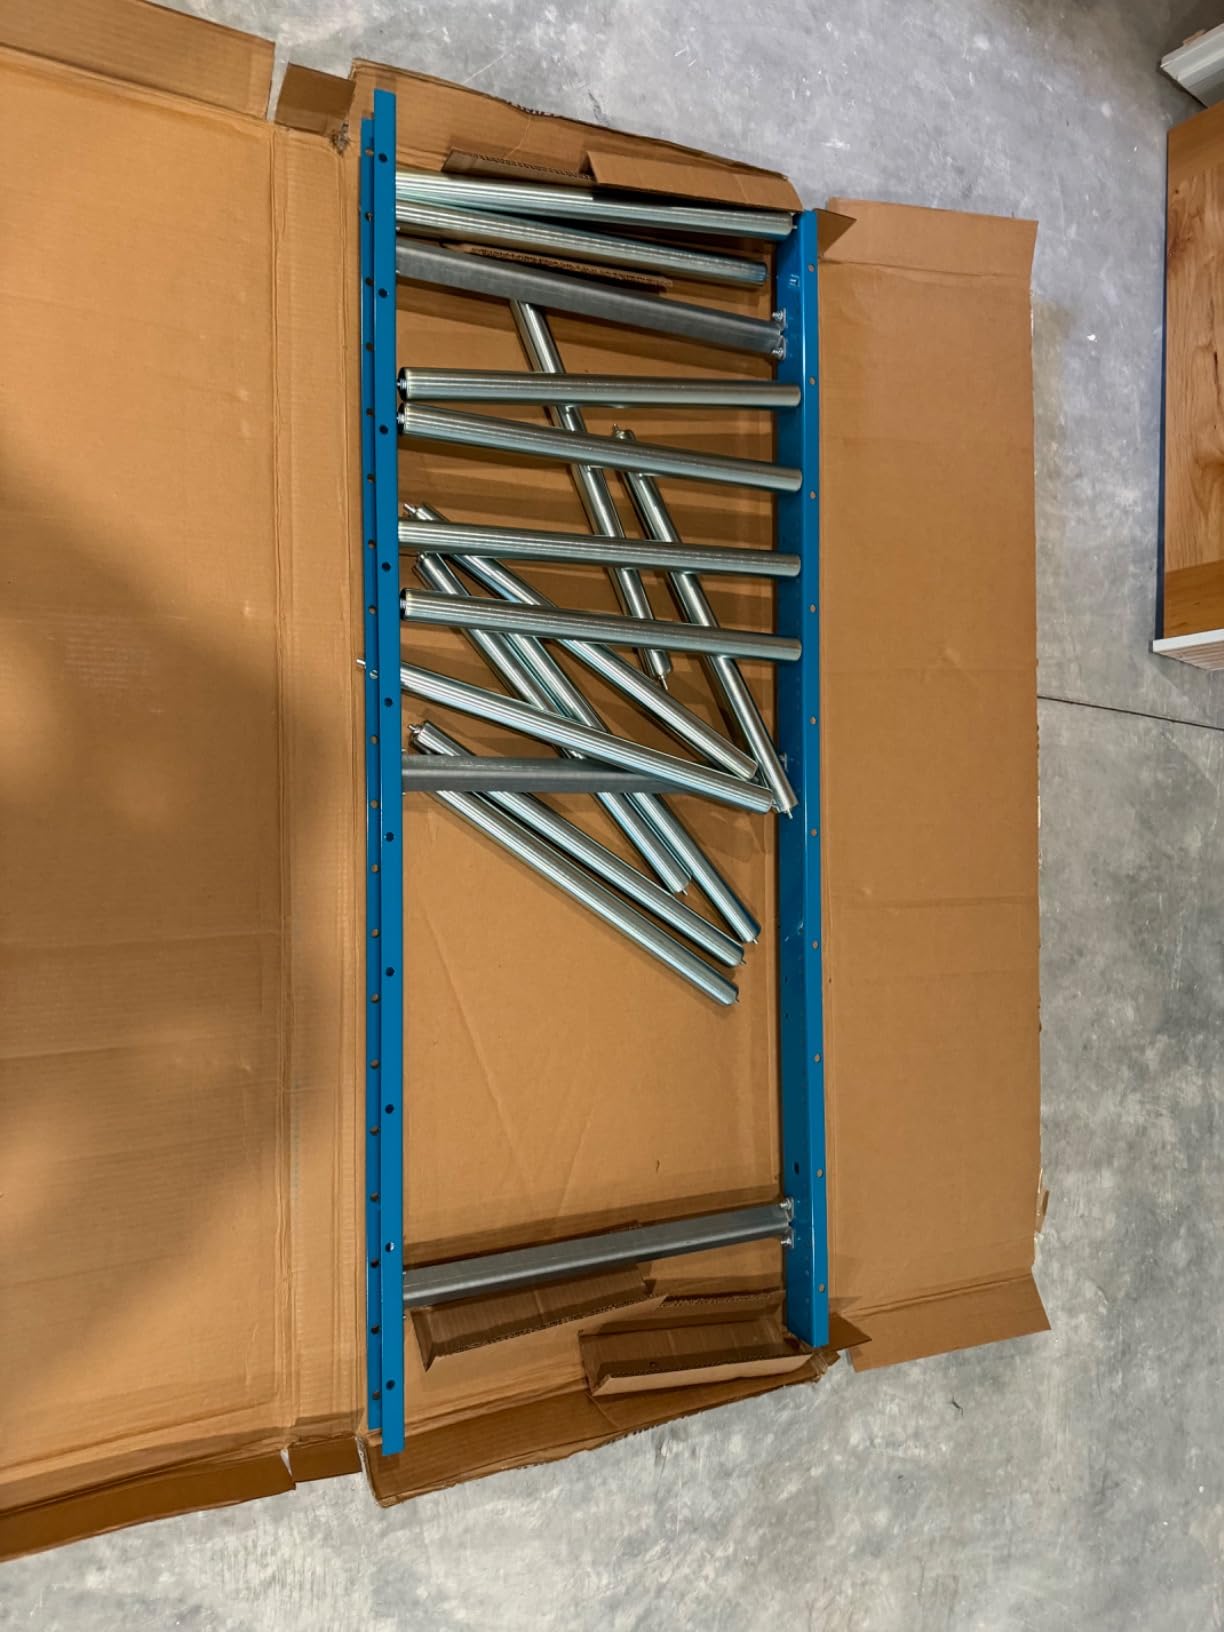
Build quality is solid for the price band. The 2-1/2 inch deep powder-coated steel frame has taken a few bumps from my pallet jack without bending, and the galvanized rollers have not rusted even after a sweaty summer near the loading dock. I did have one shipment arrive with a slightly bowed cross member, and that is a fair complaint to flag, but a pair of leg stands straightened it out in ten minutes.
Setup was effectively zero. It came pre-assembled, I dropped it on its support stands, angled the run about 3 degrees, and it has been moving product ever since. If you are new to conveyor sortation and want a section you can drop into an unloading bay, dock door, or pick-and-pack line, this is the safest first buy.
How it integrates into a sortation line
I run the Ultimation 5-footer downstream of a scan tunnel feeding parcel hubs. It works as the takeaway conveyor after a tilt-tray divert, and as the lead-in for a small manual put-wall. Because each section bolts to the next, you can scale from a 5 ft starter run to a 20 ft gravity line in an afternoon without buying specialty hardware.
Where the design pushes back
The only real limitation is the lack of diverts. This is a pure through conveyor, not a sorter. If you need automatic routing to specific lanes, you are stepping into cross-belt, tilt-tray, or pusher territory. For pure point-to-point product movement, though, it is hard to beat.
2. Ultimation 3 ft Light-Duty Gravity Roller Conveyor
Ultimation Light-Duty Gravity Conveyor, Rollers & Frames – 24″W x 3’Lx 6″C
300 lb capacity
24 inch width
1.5 inch galvanized rollers
22 lb frame
Pros
- Light enough to carry one-handed
- Modular design links to longer runs
- Same roller quality as the 5 ft version
- Footprint fits between dock doors
- Good value per linear foot
Cons
- Lower load rating than the 5 ft version
- Frame alignment inconsistencies on some shipments
- Not a stand-alone sorter
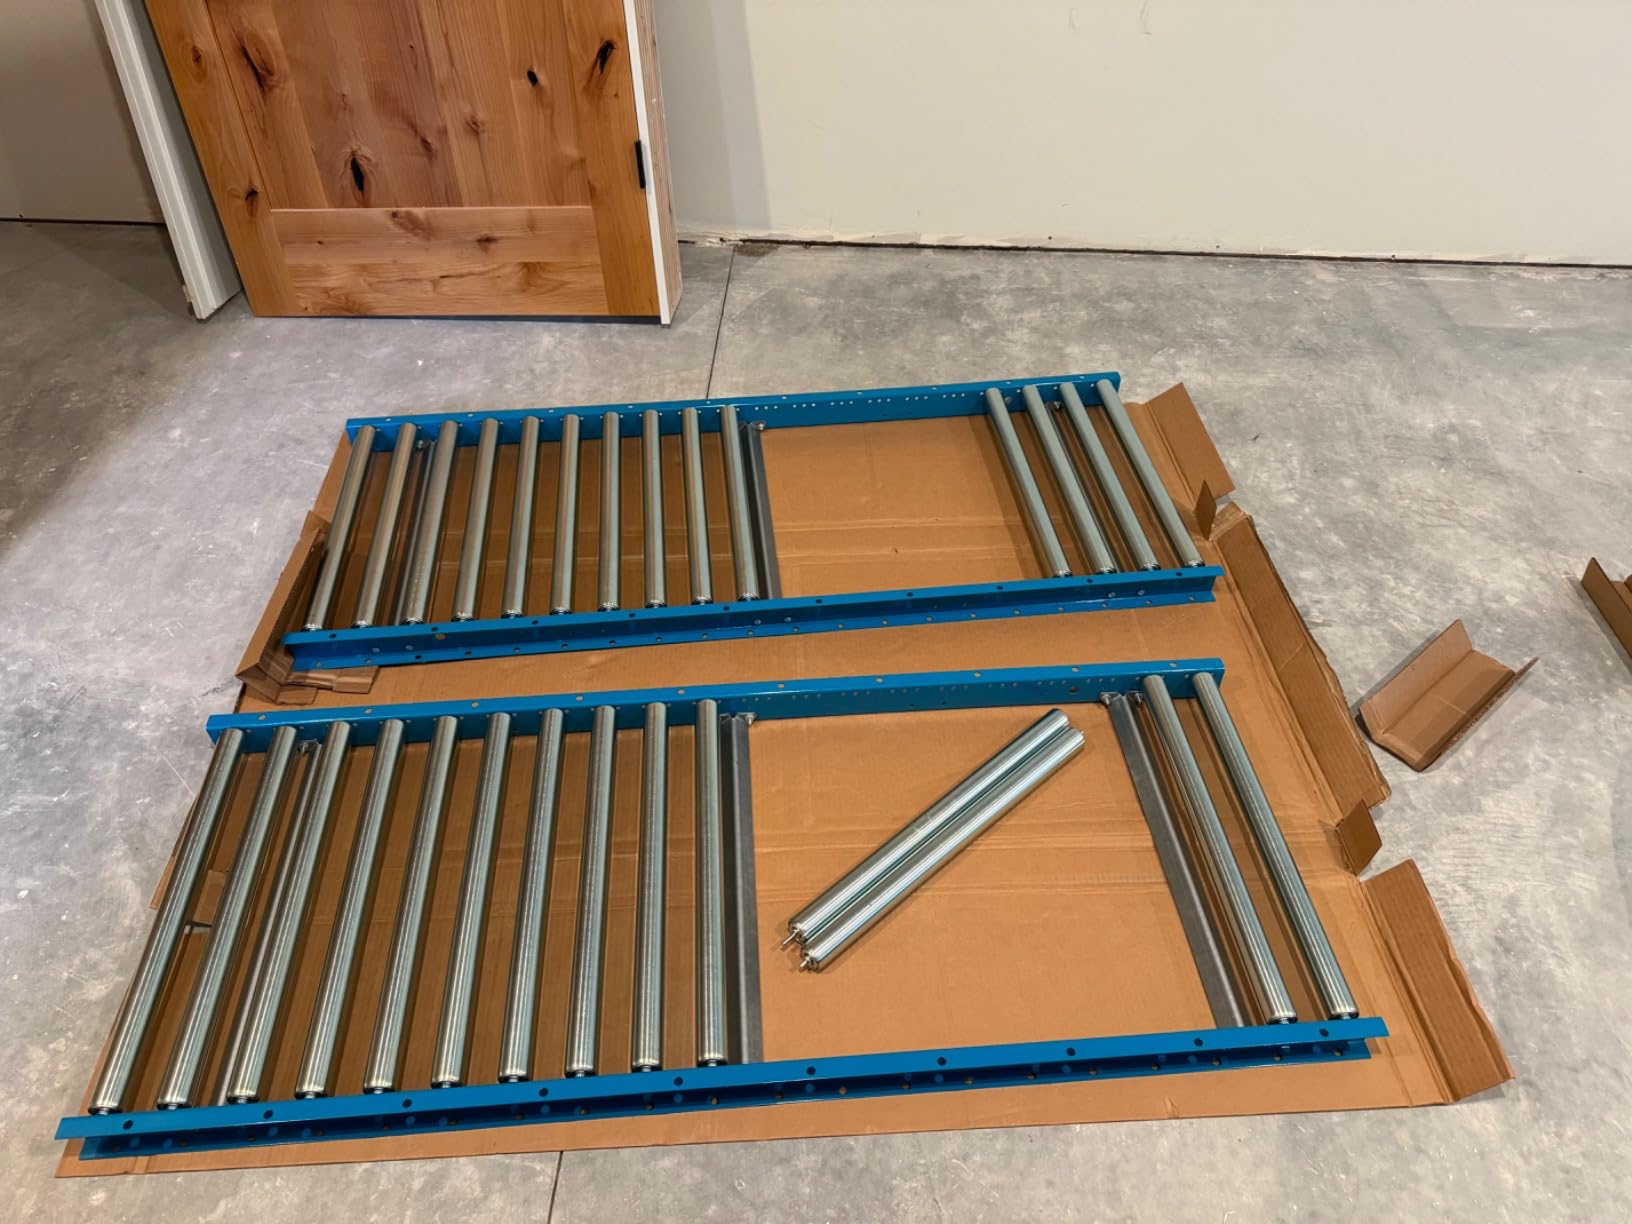
The Ultimation URS14G-24-6-3 is the short cousin of the EDITOR’S CHOICE above, and it lives at the end of my pack bench. I drop 30 to 60 lb cartons off the bench, they roll to a tote, and I am done. At 22 lb per section, even our newest hire can reposition it without asking for help.
For warehouse sortation on a budget, this is the most practical entry point I have found. The 1.5 inch galvanized rollers are the same spec as the heavier unit, and the 300 lb fully supported capacity covers everything we ship out of the small-warehouse end of the building. Reviewers on r/supplychain consistently call out that “good enough” gravity sections are a smart buy when you do not yet know your peak throughput, and I agree.
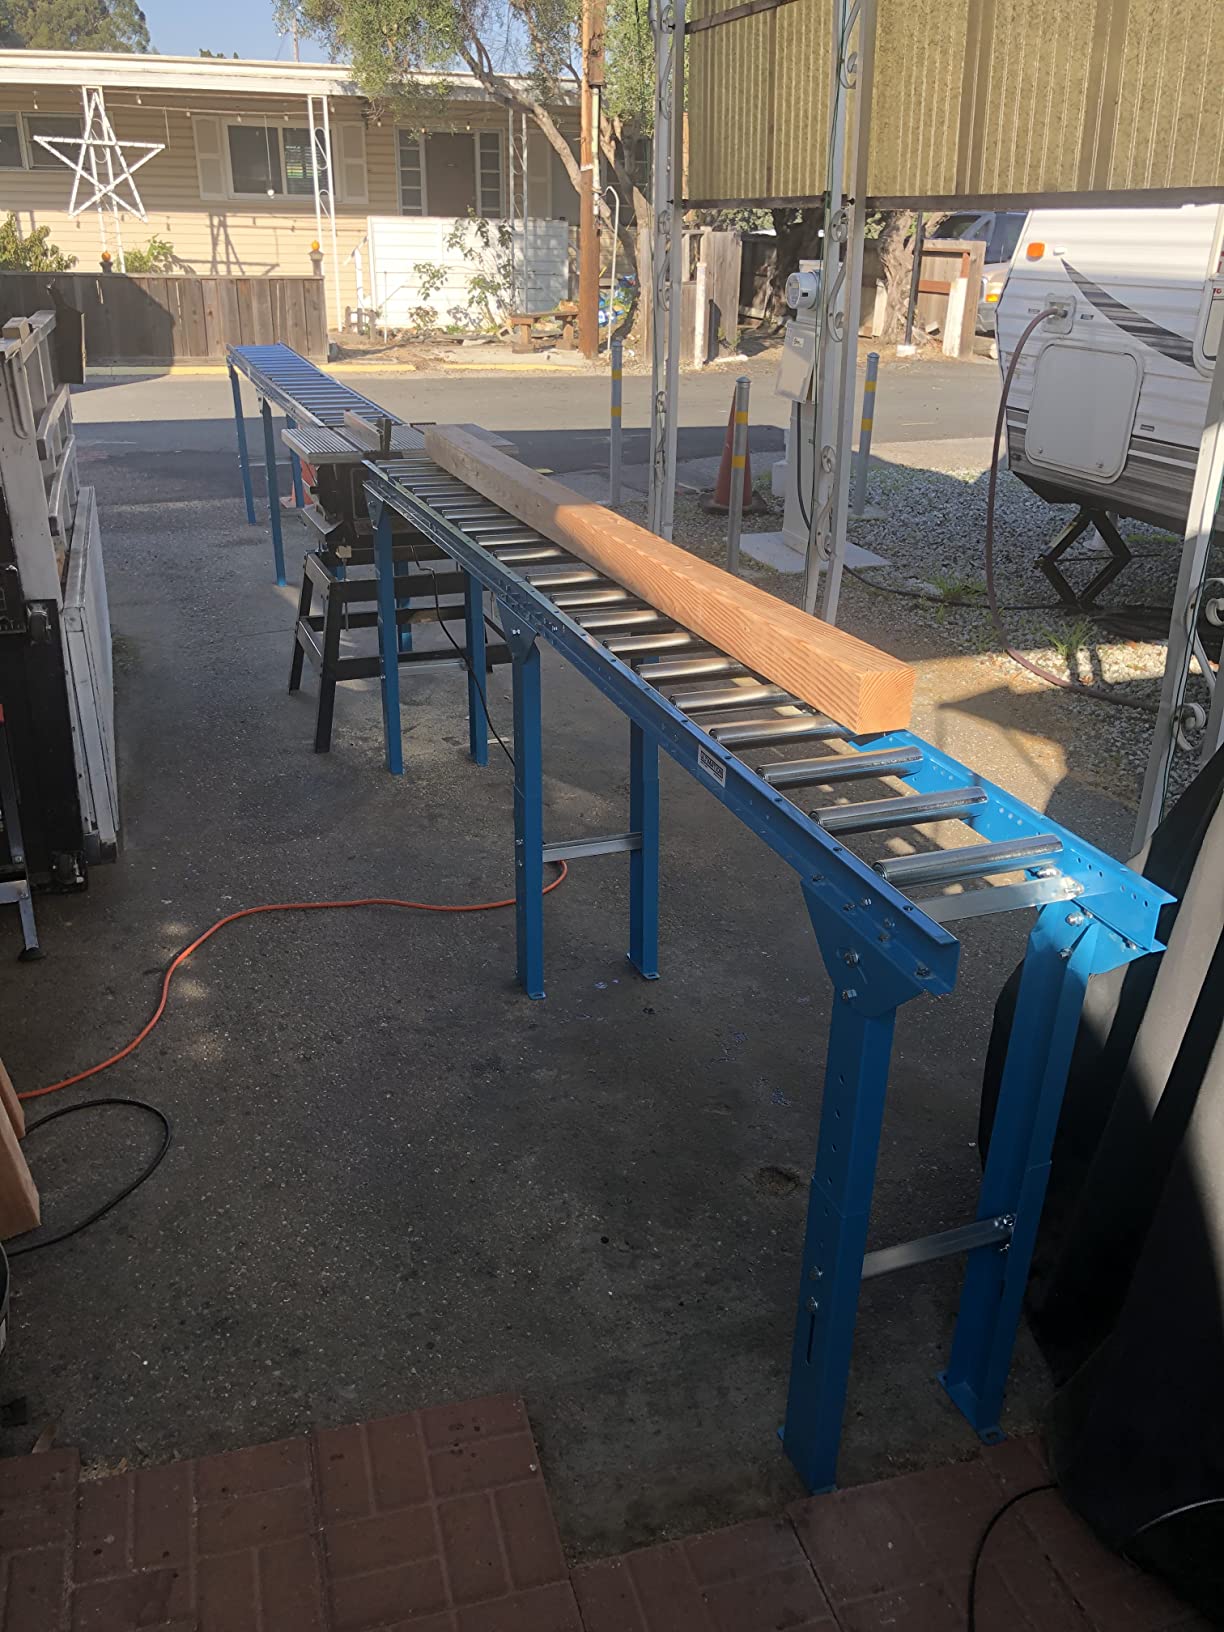
The 6 inch roller centers are wider than the 3 inch centers on the 5 ft unit, which means smaller boxes roll a touch less smoothly. In practice this only matters for items smaller than about 6 inches in their longest dimension. For typical 12 to 24 inch cartons, the 6 inch centers actually reduce the chance of a small box catching between rollers.
My favorite use is bridging a 3 ft gap between a scale and a label printer. The short run keeps the line compact, and because it hooks to other Ultimation sections, I can extend it to a 9 ft or 12 ft gravity run in a few minutes when a project demands it.
Who this section is built for
Owners of small warehouses, mobile sortation setups, or anyone running a pick-and-pack station that needs a short product takeaway. The price-to-foot ratio is hard to beat, and the build is honest for the money.
Where it runs out of headroom
If your operation needs to handle full pallets, 55-gallon drums, or anything over 300 lb fully supported, step up to the 5 ft Ultimation or a powered roller line. This is a small-parcel, light-carton section.
3. VEVOR 59 Inch Motorized PVC Belt Conveyor
VEVOR Belt Conveyor, 59 x 7.8 inch Conveyor Table, Stainless Steel Motorized Belt Conveyor PVC Belt Anti-Static Adjustable Speed (Double Guardrail)
30 to 120 RPM
59 inch belt
201 stainless steel
Anti-static PVC
Pros
- Adjustable speed for different product flows
- Anti-static PVC belt suits electronics work
- Overheat protection on the motor runs cool
- Stainless frame wipes down clean
- Bi-directional operation is genuinely useful
Cons
- Some units arrive damaged in shipping
- Build inconsistency between batches
- Occasional missing bolts or hardware
- Not rated for heavy shop duty
Power changes everything. The VEVOR PDSSJSJLK59 is the first motorized conveyor I added to my sortation setup, and it immediately doubled throughput on the line feeding my testing station. The 30 to 120 RPM stepless speed adjustment lets me run slow for QC inspection and ramp up to 120 RPM when I am just ferrying boxes from A to B.
For conveyor sortation systems at the small-warehouse end of the market, a powered belt is the missing link between a passive gravity line and a full industrial sorter. I have used the VEVOR as the induction conveyor feeding a small pusher diverter, and the consistent belt speed made the diverter timing reliable.
The 201 stainless steel frame is a real plus. I run a small electronics QC bench downstream of the line, and the anti-static PVC belt has not produced a single static discharge event in three months. The motor’s automatic overheat cutoff at 88 degrees C and restart at 80 degrees C is reassuring for long shifts.
Build quality is mixed. My unit arrived with a slightly bent guardrail that I straightened in five minutes. One of my neighbors who bought the same saw reported a missing bolt bag, which is the kind of quality inconsistency you should expect with this price point. For light industrial and assembly line duty, it earns its keep.
Best fit for production environments
If you are moving small packaged goods through a packaging factory, pharmaceutical line, food packing operation, or auto parts station, the VEVOR’s stainless build and adjustable speed cover the bases. For heavier general warehouse sortation, look at the heavy-duty gravity lines or a powered roller unit instead.
When the VEVOR is the wrong tool
Operators on r/ManufacturingPorn warn that under-spec powered conveyors fail at the drive roller, not the belt. The VEVOR is a light industrial unit. If you need a 24/7 production line, step up to an enterprise-class powered conveyor from Hytrol, Honeywell Intelligrated, or TGW.
4. LXSEHN Foldable Portable Gravity Roller Conveyor
Conveyor Roller for Werehouse Unload,Foldable Unpowered Conveyor Belt Table
120 kg capacity
Folds to 39 inches
6 horizontal shafts
-30C rated
Pros
- Fits in a car trunk when folded
- 29 lb total weight is genuinely portable
- Operates in frozen warehouses at -30C
- Multiple sections link for longer runs
- Setup is one minute
Cons
- Plastic rollers can pop off under heavy use
- Frame quality varies
- Slope speed can run away with light items
- Not built for daily commercial duty
There is a place in every sortation toolkit for a conveyor that folds up and rides in the back of a truck. The LXSEHN DODBBJEBV-WHITE is that tool for me. I have used it to unload a refrigerated truck in -20C weather, and it kept rolling without a hiccup. The -30C operating rating is not marketing fluff.
When warehouse sortation has to be mobile, this foldable conveyor earns its slot. I have also pulled it out for kayak and boat loading at a friend’s shop, which is the kind of versatility that makes a piece of equipment worth its storage footprint. Reviewers consistently praise the foldable design for fitting in standard car trunks.
The 120 kg capacity without the middle support column is enough for cartons up to about 265 lb. With the support column in place, the load rating climbs. For warehouse sortation duty, I treat it as a 200 lb unit, and it has been fine.
Quality control is the soft spot. Two of the plastic wheels popped off during my first hour of use, and I had to snap them back in. A few reviewers on Amazon reported similar issues. If you buy this, expect to spend ten minutes seating the wheels firmly the first day.
Where portability pays off
Mobile sortation at pop-up distribution events, satellite warehouses, seasonal overflow operations, or any DC that needs to reconfigure its floor plan monthly. The foldable footprint is the headline feature.
Where this conveyor runs out of use cases
Daily high-volume warehouse sortation in a fixed location. The plastic rollers and lightweight frame will not survive the abuse of a year-round carton flow. Treat this as a tactical, mobile tool rather than a primary line.
5. Ultimation Staggered Skate Wheel Flow Rail
Ultimation Roller Conveyor Flow Rail – Heavy Duty Gravity Conveyor with Staggered Plastic Skate Wheels for Efficient Pallet, Carton & Material Handling, Portable System – 5′ Galvanized Steel Rail
1000 lb capacity
5 foot galvanized rail
Staggered plastic skate wheels
12 lb section
Pros
- Galvanized frame resists corrosion
- Staggered wheels handle odd-sized cartons
- Modular sections join seamlessly
- No power needed
- Easy to install and reconfigure
Cons
- Very small review base
- Wheels can wear under heavy sliding loads
- Not a stand-alone sorter
Skate wheel flow rails solve a problem that gravity rollers cannot: cartons of mixed width. The Ultimation ULT-FRP-GALV-5S uses staggered plastic skate wheels that handle everything from a 6 inch cube to a 24 inch carton without the rollers losing contact. I have it running between a stretch wrapper and a pick line, and the flow never stalls.
For pallet flow and carton flow at the small-warehouse end of conveyor sortation, this is the right tool. Operators on r/logistics often recommend flow rails for any pick module where product size varies by order, and the staggered wheel layout is the standard answer.
Build quality impressed me. The galvanized steel frame is heavier-gauge than the price suggests, and the plastic skate wheels have held up to months of constant carton abuse. The 1000 lb fully supported capacity is honest for the duty cycle I run.
The only real caution is the small review base. Five reviews is not enough to call long-term durability. So far, my own experience has been positive across two sections installed six months back.
When to reach for a flow rail
Carton flow between operations, lightweight pallet flow, gravity-fed pick modules, and any place you want zero-power product movement. If you have ever lost time because a small box caught between rollers on a traditional gravity conveyor, the staggered skate wheels solve that.
When a flow rail is not the right pick
Flat-bottomed totes and bins roll poorly on skate wheels because the contact patch is small. For those, go back to a gravity roller conveyor. Flow rails are optimized for cardboard cartons.
6. Ultimation Adjustable Height Roller Table Set
Ultimation Gravity Conveyor Roller Table Set 18″ Wide x 5′ Long with 1.9″ Steel Rollers, Outfeed Support System for Saw Stand, Workshop or Unload Station, Adjustable Legs, Material Handling
265 lb per roller
18 inch width
Adjustable 22 to 28 inch height
94 lb with stands
Pros
- Complete set with support leg stands included
- Adjustable height fits saws and benches
- 1.9 inch rollers handle heavier cartons
- 16 gauge steel frame is stiff
- Powder-coated Ultimation Blue finish
Cons
- 94 lb total weight is less portable
- Very small review base
- Not a motorized sorter
When you need a conveyor that stands on its own and adjusts to match your bench height, the Ultimation URS19G18-6-5-Set is the cleanest answer I have tested. The two adjustable leg stands are included, and the height range from 22-1/16 inches to 28-1/16 inches covers every table saw and outfeed bench in my shop.
For warehouse sortation feeding a workbench or saw station, this is the most “drop in and go” option on the list. The 1.9 inch galvanized rollers handle heavier workpieces than the 1.5 inch rollers on the lighter gravity models, which is the real reason I bought a second one for a different line.
Build is substantial. The 16 gauge powder-coated steel frame does not flex under load, and the Ultimation Blue finish has resisted scratches in my shop better than the galvanized finish on the other Ultimation models. The 265 lb per roller capacity is overkill for most applications, but it means the conveyor will not sag even when a heavy slab of plywood rides it.
The honest warning is the small review base. Two reviews is a tiny sample. That said, both my unit and the second one I bought for a partner have performed without issue across several months of weekend and weekday use.
Best use cases for a leg-stand conveyor
Workshop outfeed, sawmill and lumber operations, mobile pack benches, anywhere you need an adjustable-height surface that moves product. The included stands remove the most common headache of buying a separate stand kit.
Where this conveyor falls short
If you need to move it daily, the 94 lb weight is a real penalty. For a stationary installation at a fixed height, it is a great pick. For daily repositioning, the lighter gravity rollers are friendlier.
7. Moonshan 39 Inch Desktop PVC Belt Conveyor
Moonshan Belt Conveyor 39 inch Conveyor Desktop Version Step-Less Speed Adjustment PVC Belt Conveyor for Packaging Factory, Production Line, Home
11 lb capacity
39 inch PVC belt
Stepless speed control
Silent motor
Pros
- Stepless speed control is smooth
- Silent motor runs quiet on a desk
- Compact desktop footprint
- Waterproof PVC belt wipes clean
- Easy to assemble
Cons
- 11 lb load limit rules out heavier work
- 6 inch belt width restricts item size
- Not a production-line conveyor
Desktop conveyor sortation is a niche, but if you run a small e-commerce packing desk or a craft production line, the Moonshan TT-63-MLY is the right size. At 39 inches long and 6 inches wide, it sits on a workbench between a label printer and a shipper box without dominating the surface.
The stepless speed control is the headline feature. I can dial it down to a crawl for QC checks or run it at full tilt for a packaging sprint, and the response is instant. The silent motor is genuinely quiet, which is the difference between a tool that lives on my desk and one that gets banished to the back room.
The waterproof PVC belt has been easy to wipe clean, even after a glue spill. Setup took about fifteen minutes, and the included brackets let me angle the conveyor down into a collection bin for a small assembly run.
The honest constraint is the 11 lb load capacity and 6 inch belt width. This is a desktop tool, not a warehouse sortation conveyor. If you try to push a standard 12 inch carton through it, the belt will struggle. For small parts, vials, sachets, and lightweight packaged goods, it is excellent.
Where the Moonshan shines
Craft production, small parts packaging, laboratory sample handling, lightweight e-commerce packing desks, and any desktop application where quiet operation matters. It is also a great training tool for showing staff what a powered conveyor does before you scale to a full warehouse line.
Where this conveyor does not fit
Standard cartons, parts over 11 lb, or any application where you need to feed a downstream sorter. The desktop format is the entire point, but it is also the limit.
8. Global Industrial Portable Flexible Expandable Conveyor
Global Industrial 18″W Portable Flexible & Expandable Conveyor, 6’2″-24’8″L
Expands 6 inch to 24 inch
175 lb per foot
4 inch swivel casters
315 lb unit
Pros
- Expands from 6 ft 2 in to 24 ft 8 in
- Hook couplers link to additional conveyors
- Swivel casters roll on standard warehouse floors
- 175 lb per foot load capacity
- Includes box stop and couplers
Cons
- 315 lb unit weight requires two people to move
- Small review base
- Premium price for a flexible conveyor
The Global Industrial 168110 is the most flexible conveyor on this list, literally. It expands from a compact 6 ft 2 in to a full 24 ft 8 in, which means a single piece of equipment covers both truck unloading and dock-to-zone product movement. For warehouse sortation that has to flex with the day, that is a real advantage.
I use the 168110 to bridge the gap between my dock door and the pick line on days when the dock layout changes. The swivel casters roll smoothly on sealed concrete and even on the slightly uneven surface of our older warehouse. The hook couplers let me daisy-chain a second conveyor when a single run is not long enough.
The 175 lb per foot load rating is honest for typical carton flow, and the box stop keeps product from rolling off the end when the conveyor is angled for gravity flow. I have run 50 lb reship cartons across the full 24 ft extension without flex or sag.
The honest trade-offs are weight and price. At 315 lb, this is a two-person move even with the casters. And the price is meaningfully above the gravity roller alternatives. For a fixed conveyor line, a stationary roller or belt unit is the better buy. For a flexible layout, the Global Industrial earns its slot.
Where a flexible expandable conveyor shines
Truck and trailer unloading, dock doors of varying heights, seasonal overflow operations, and any warehouse that reconfigures its floor plan more than once a quarter. The flexibility is unmatched by rigid gravity or belt sections.
Where it does not fit
Fixed high-volume sortation lines, cleanroom or food-grade environments where the wheeled base is a contamination risk, and operations that need to feed a downstream sorter with precise indexing. This is a flexible run, not a precision sorter.
How to Choose the Right Conveyor Sortation System
The best conveyor sortation systems for warehouses are the ones matched to your throughput, your product mix, and your floor plan. Before you buy, walk your warehouse and answer five questions. First, what is your peak throughput in cartons per hour, and which days of the week see the surge. Second, what is the size and weight range of the items you are sorting. Third, how much linear footage can you dedicate to a sort line. Fourth, do you need automated diverts, or is manual routing acceptable. Fifth, what is your integration story with your existing WMS or WCS.
If you are processing 500 orders per hour or more and you have a fixed layout, you are firmly in cross-belt sorter, tilt-tray sorter, or sliding shoe sorter territory from Hytrol, Honeywell Intelligrated, Dematic, Beumer, Interroll, FMH Conveyors, TGW, Element Logic, or Vanderlande. Those are the enterprise conveyor sortation systems that handle 10,000 to 25,000 units per hour at 99%+ accuracy, and they are the right answer for high-volume 3PL and parcel operations. If you want a closer look at factory conveyor hardware, our guide to conveyor systems for factories covers the production side.
If you are below 500 orders per hour, or you need to bridge a manual pick line to a packing bench, the gravity roller and motorized belt sections in this guide are the right tier. Within that tier, match the conveyor to the load: 1.5 inch galvanized rollers handle most small-carton duty, while 1.9 inch rollers step up to heavier workpieces. Powered belt conveyors with adjustable speed are the right pick when you need throughput consistency, and flexible expandable conveyors are the right pick when your layout changes monthly.
Match the sorter type to the application
Cross-belt sorters dominate apparel and GOH distribution because they handle garments gently and can pack diverts close together. Tilt-tray sorters are the workhorse for high-volume parcel post and 3PL operations, where lightweight items need to fan out to many destination chutes. Sliding shoe sorters are the go-to for mixed-size case sortation in grocery and retail DCs. Pop-up wheel sorters handle cartons in mid-volume operations. Pusher sorters are the budget answer for low-throughput cases. Bomb bay sorters win on compact footprint in mezzanine installations. ARB sorters, patented by Intralox, run gentle sortation for fragile or irregular items.
For your first purchase at the small-warehouse end of the market, I would start with two 5 ft Ultimation gravity rollers, one VEVOR motorized belt, and one Global Industrial flexible unit for dock work. That covers most loading, unloading, and pack-bench scenarios. For warehouse sortation expansion later, look at FMH Conveyors LITESORT for modular conveyor sortation, or TGW Ermanco for European-engineered lines. If you are building out a mezzanine picking operation, our mezzanine systems guide covers the structural side of that project.
WMS and WCS integration reality
Operators on r/Warehousing consistently flag WMS and WCS integration as the slowest, most expensive part of any conveyor sortation project. The hardware is the easy part. The integration is where timelines slip and budgets balloon. For an enterprise sorter from Hytrol, Honeywell Intelligrated, or Dematic, plan for a 12 to 26 week implementation cycle, with most of that on the software side. For the small-warehouse gear on this list, integration is usually a barcode scan and a label print, which is much faster.
Total cost of ownership and maintenance
Most competitor guides hand-wave the cost question. Here is a realistic framework. Capex is the conveyor hardware plus any diverts, scanners, and integration hardware. Installation is typically 10 to 20 percent of capex for the small-warehouse gear, and 30 to 50 percent of capex for a full sorter line including electrical, controls, and rigging. Integration with WMS or WCS adds another 15 to 30 percent on top of hardware, especially if your existing stack is on Manhattan, Blue Yonder, or SAP EWM. Annual maintenance and spare parts for a full sorter line typically lands at 3 to 5 percent of capex per year. Expected life for a properly maintained sorter is 15 to 20 years, so the lifetime cost is heavily back-loaded.
Refurbished versus new sortation
Refurbished sortation gear from integrators like SJF can cut capex by 40 to 60 percent, but the trade-offs are real. Older Hytrol and Intelligrated sorters may have legacy scan tunnel integration that does not speak modern WMS protocols, and spare parts lead times for 5+ year old installs can stretch to weeks. For a first sortation line where uptime is critical, new gear with a vendor uptime SLA is the safer buy. For a non-critical secondary line, refurbished sortation is a legitimate option. If you are looking at related industrial gear for a mining or aggregate operation, our conveyor belts for mining guide covers the heavy industrial end.
Industry-specific fit
Apparel and garment-on-hanger distribution favors cross-belt sorters from Beumer, Interroll, or Hytrol for gentle handling. E-commerce parcel hubs favor tilt-tray sorters from Honeywell Intelligrated or Dematic for high divert density. Grocery distribution centers favor sliding shoe sorters from FMH Conveyors or TGW for mixed-size case handling. 3PL operations favor modular conveyor sortation from FMH LITESORT or Vanderlande for layout flexibility. Returns processing favors bomb bay sorters for compact mezzanine sortation. If you run a small operation that needs climate control or heating in the warehouse, our infrared heaters guide is worth a read. And if you are in food service, our conveyor pizza ovens guide covers a related niche.
Future trends in conveyor sortation
AI-driven sortation is starting to appear in mid-tier installations, with vision systems replacing mechanical scan tunnels. AMR integration is the bigger shift, with autonomous mobile robots feeding sortation lines instead of traditional conveyors. Modular designs from FMH Conveyors and Vanderlande let facilities add diverts and reconfigure lines without ripping out the floor. Sustainability is becoming a procurement criterion, with energy recovery and regenerative drives cutting the sortation line power draw. None of these trends matter for the small-warehouse gear on this list yet, but if you are planning a multi-year roadmap, factor them in.
Frequently Asked Questions
What are the different types of conveyor systems used in warehouses?
The main warehouse conveyor types are belt conveyors for general transport, roller conveyors for carton flow, chain conveyors for heavy pallets, and sortation conveyors that divert product to specific destinations. Within sortation specifically, the leading types are cross-belt sorters for gentle garment handling, tilt-tray sorters for high-volume parcel post, sliding shoe sorters for mixed-size case handling, narrow belt sorters, pop-up wheel sorters, pusher sorters, bomb bay sorters, and ARB (Activated Roller Belt) sorters for fragile items.
What are conveyor sorting systems?
A conveyor sorting system is an automated material-handling setup that identifies, transports, and diverts packages or cartons from a main conveyor line to their correct downstream destination. Items travel along an induction conveyor, are scanned by barcode, RFID, or vision systems, and at the correct divert point a mechanism fires to push the item off onto a designated takeaway lane. The result is faster, more accurate order fulfillment than manual sorting can deliver.
What are the different types of conveyor sorters?
The main conveyor sorter types are cross-belt, tilt-tray, sliding shoe, narrow belt, pop-up wheel, pusher, bomb bay, and ARB (Activated Roller Belt). Cross-belt handles apparel and GOH gently, tilt-tray handles high-volume parcel post, sliding shoe handles mixed-size case sortation, narrow belt handles mid-rate applications, pop-up wheel handles cartons, pusher handles low-throughput cases, bomb bay handles mezzanine sortation, and ARB handles fragile or irregular items.
What is a cross belt sorter?
A cross-belt sorter is a conveyor loop fitted with small motorized belts across each carrier that fire perpendicular to the direction of travel to push an item off the loop into a takeaway chute. It is the quietest sorter type, handles garments and fragile items gently, and can pack diverts close together for high-density sortation. Common manufacturers include Hytrol, Beumer, and Interroll.
What is a Hytrol conveyor?
Hytrol is one of the largest North American conveyor manufacturers, headquartered in Jonesboro, Arkansas. They build gravity rollers, powered belt conveyors, and a full sortation line including pivot wheel sorters, horizontal belt sortation, and high-speed sortation. Their E24, E27, and accumulation conveyor lines are common in distribution centers, and their sortation products are popular at the small and mid-tier end of the warehouse sortation market.
Who are the top 10 conveyor manufacturers in the world?
The leading conveyor manufacturers globally include Hytrol, Honeywell Intelligrated, Dematic, Beumer, Interroll, FMH Conveyors, TGW, Element Logic, Vanderlande, and Swisslog. Hytrol is the largest North American conveyor manufacturer. Honeywell Intelligrated, Dematic, and Vanderlande dominate enterprise sortation. Beumer is strong in cross-belt and parcel. Interroll builds drum motors and modular conveyor platforms. FMH Conveyors specializes in modular sortation with their LITESORT line. TGW and Swisslog cover European-engineered systems. Element Logic focuses on ASRS and integrated fulfillment.
Who are Hytrol’s main competitors in conveyor systems?
Hytrol’s main competitors in conveyor systems include Honeywell Intelligrated, Dematic, TGW Ermanco, FMH Conveyors, Beumer, Interroll, and Vanderlande. In the sortation-specific market, Hytrol competes with Honeywell Intelligrated and Dematic at the enterprise tier, with FMH Conveyors and TGW in the modular mid-tier, and with Interroll and Beumer in the cross-belt and tilt-tray segment. Smaller competitors include Bastian Solutions, OPEX, and Material Handling Systems.
Final Verdict: Which Conveyor Sortation System Should You Buy
If you need a single, dependable section to drop into a small warehouse, dock door, or pack bench right now, the Ultimation 5 ft Galvanized Gravity Roller Conveyor is the EDITOR’S CHOICE and the safest first buy on this list. It pairs honest 1000 lb capacity with the build quality to survive years of daily carton flow.
If budget is the constraint and you only need a short run to bridge a bench, the Ultimation 3 ft Light-Duty Gravity Roller delivers the same roller quality at a lower price and a lighter carry weight. Add the VEVOR motorized belt when you need powered throughput, and the Global Industrial flexible expandable conveyor when your dock layout changes monthly. Together those four cover most of what a small or mid-size warehouse actually needs before stepping up to enterprise cross-belt, tilt-tray, or sliding shoe sortation from Hytrol, Honeywell Intelligrated, Dematic, or Beumer.
For high-volume operations above 500 orders per hour, plan a real vendor evaluation with the major conveyor sortation manufacturers, get reference customers in your industry, and budget 12 to 26 weeks for full WMS or WCS integration. For everything below that bar, the gear on this list is the practical answer, and the right starting point for the best conveyor sortation systems for warehouses in 2026.